Engineering-Grade Valve Solutions — Top Showcase
Explore our heavy-duty industrial valves manufactured for high-reliability municipal water networks, power plants, and chemical processing facilities.
1. Executive Analysis: The Mechanics of Custom Non-Rising Stem (NRS) Gate Valves
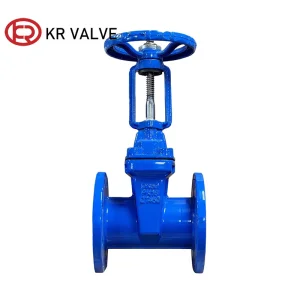
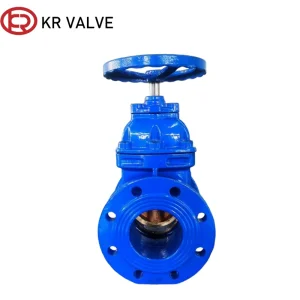
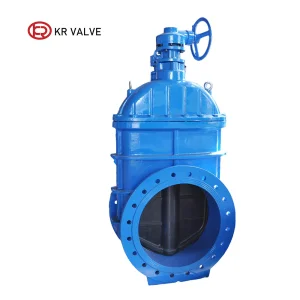
In high-density civil infrastructure and subterranean fluid transport systems, spatial efficiency and total operational isolation are paramount. The Non-Rising Stem (NRS) Gate Valve—also designated as an inside-screw gate valve—stands as the definitive engineering solution where vertical installation space is strictly limited.
1.1 Kinematic Differentiation: NRS vs. OS&Y (Outside Screw & Yoke)
Unlike Rising Stem (OS&Y) valves where the stem lifts linearly out of the bonnet during actuation, a Non-Rising Stem Gate Valve features an internal stem thread engaged directly into the wedge nut inside the valve chamber. As the handwheel or electric actuator rotates the stem, the stem turns in place without vertical displacement, driving the wedge up or down along the internal thread pitch.
This design eliminates external stem height variation during operation, preventing damage to external threads from aggressive soil chemistry, moisture, UV radiation, and atmospheric particulate contamination in underground pits, compact plant rooms, and buried direct-burial service.
| Performance Dimension | Non-Rising Stem (NRS) Design | Rising Stem (OS&Y) Design | Engineering Selection Threshold |
|---|---|---|---|
| Vertical Envelope Requirement | Zero extra clearance required above handwheel | Requires 100% stroke height extension space | NRS preferred for underground vaults & tight piping galleries |
| Stem Thread Exposure | Encapsulated in flow medium/grease chamber | Exposed to external atmosphere & ambient dust | NRS prevents environmental stem thread corrosion |
| Sealing Architecture | Vulcanized EPDM/NBR Resilient Seated Wedge | Metal-to-Metal or Soft Seated Options | Resilient NRS achieves ISO 5208 Rate A zero-leakage shutoff |
| Visual Position Indication | Requires integrated optical/electronic gear indicator | Inherent (stem physical height shows stroke position) | NRS requires magnetic or mechanical top indicators for SCADA |
| Direct Burial Capability | Superior (supports extension spindles & valve boxes) | Poor (requires heavy external protection tubes) | NRS is standard for municipal water main distribution |
2. Advanced Material Science & Structural Engineering
Custom non-rising stem gate valves engineered by modern ISO 9001 certified suppliers utilize advanced metallurgy, specialized elastomer vulcanization, and low-friction thrust bearing assemblies to achieve a 50-year service life in aggressive underground networks.
Ductile Iron Body Metallurgy
Forged from high-tensile Ductile Iron (EN-GJS-450-10 / ASTM A536 65-45-12), offering superior yield strength (>310 MPa) and impact resistance compared to standard gray cast iron (GG25), preventing fractures under severe water hammer hydraulic surges.
EPDM / NBR Encapsulated Wedge
The ductile iron gate wedge is fully vulcanized with high-purity EPDM or NBR rubber through high-temperature compression molding. The rubber memory resists permanent deformation, providing bubble-tight bi-directional sealing even when medium contains solid suspended debris.
Stem Threading & Bearing System
Forged Stainless Steel stems (SS420 / SS316 / Duplex 2205) paired with solid bronze (CC491K) stem nuts. Cold-rolled stem threads deliver a smooth surface roughness (Ra < 0.4 µm), reducing operating torque by over 35% compared to cut threads.
Custom NRS Gate Valves engineered for underground potable water mains undergo electrostatic thermal application of non-toxic, blue Fusion-Bonded Epoxy (FBE) coating conforming to DIN 30677-2 and GSK specifications. Coating thickness is maintained at a minimum of 250 µm, ensuring 100% isolation of raw metal from aggressive soils and tuberculation-inducing fluid chemistry.
3. China Smart Manufacturing: Supply Chain Resilience & Precision Testing
Modern Chinese valve manufacturing facilities have transitioned from manual labor-intensive operations to automated Industry 4.0 smart foundries. This technological migration guarantees dimensional repeatability, structural purity, and cost efficiency for international OEM partners.
Advanced Casting & Machining Matrix
- ✓ Automated Resin Sand Molding: Ensures defect-free casting structures, eliminating internal blowholes, micro-porosity, and wall thickness variations.
- ✓ 5-Axis CNC Machining Centers: Maintains precision flange drilling tolerance (ANSI B16.1, EN 1092-2) and stem bore alignment within ±0.02mm.
- ✓ Spectrometric Material Verification: Every heat batch undergoes real-time optical emission spectrometry (OES) chemical composition analysis.
100% Zero-Defect Quality Assurance Protocols
- ✓ Shell Pressure Testing: Tested at 1.5× PN rating hydrostatic pressure according to EN 12266-1 and API 598 standards.
- ✓ Low-Pressure Air Seat Test: 0.6 MPa pneumatic seat testing guarantees bubble-tight performance under low differential pressure.
- ✓ Torque Verification: Actuation torque measured electronically across full stroke to prevent stem binding under max AP pressure.
4. Macro-Industry Solutions & Fluid Application Engineering
Customized Non-Rising Stem Gate Valves serve as vital isolation control points across complex municipal, commercial, and industrial utility landscapes.
Underground Municipal Water
Directly buried in municipal water mains equipped with extension spindles and key-operated street caps, eliminating expensive manhole construction costs.
Fire Protection Lines
AWWA C515 / UL FM-compliant NRS post indicator gate valves used in fire main isolation, ensuring immediate full-bore water flow during emergencies.
HVAC & Chilled Water
Compact face-to-face dimensions (DIN 3352 F4) allow dense installation inside skyscraper baseline plant rooms and cooling tower loops.
Desalination & Marine
Customized with Duplex 2205 stems, Super Duplex wedges, and high-build epoxy coatings to withstand abrasive marine brine and salt-spray atmospheres.
5. Global Procurement Framework & Total Cost of Ownership (TCO)
EPC contractors, utility managers, and wholesale importers must evaluate total life-cycle expenditures rather than baseline purchase price alone when sourcing custom non-rising stem gate valves.
Sourcing Risk Mitigation & Documentation
Reliable Chinese suppliers provide complete EN 10204 3.1 material traceability, non-destructive testing (NDT) reports (radiographic/ultrasonic testing for heavy bodies), and third-party inspection sign-offs (SGS, TUV, Bureau Veritas) prior to vessel loading.
TCO Reduction Drivers
By specifying WRAS/NSF-certified EPDM wedges and cold-rolled stainless stems, maintenance intervals are extended from 3 years to 15+ years. Friction-free sealing prevents seat scoring, cutting pump energy losses caused by internal valve bypass leakage.
6. International Regulatory Compliance & Standardization
Global infrastructure deployment mandates compliance with stringent regional design standards and potable water hygienic directives.
Design & Face-to-Face
Manufactured strictly according to BS 5163, DIN 3352 F4/F5, EN 1074-1/2, and AWWA C515 / C509. Flange drilling customized to ANSI B16.1 Class 125/150, EN 1092-2 PN10/PN16/PN25, or JIS 10K/16K.
Hygiene & Health Certificates
Fully compliant with global drinking water toxicity mandates, holding active certifications for WRAS (UK), DVGW (Germany), NSF/ANSI 61 & 372 (USA), and ACS (France).
Pressure & Safety Directive
Certified under European Pressure Equipment Directive CE/PED 2014/68/EU and ISO 9001:2015, ISO 14001, and ISO 4501 occupational health and environmental standards.
7. Technical Roadmap & Future Outlook (2026–2035)
The evolution of custom non-rising stem gate valves is centered on digital monitoring integration, zero-PFAS eco-elastomers, and anti-cavitation internal profiling.
Phase 1: Smart-Sensored NRS Bonnet Assemblies (IoT Ready)
Integration of low-power wireless stem rotation telemetry sensors, internal pressure transducers, and acoustic leak-detection chips embedded inside the top bonnet, transmitting real-time pipeline health data to municipal SCADA networks.
Phase 2: PFAS-Free & Eco-Compliant Elastomer Formulations
Pioneering next-generation fluorine-free EPDM elastomers that eliminate forever-chemicals while retaining high ozone resistance, low compression set, and improved resistance to chloramine water treatment additives.
Phase 3: High-Torque Reduction Nano-Ceramic Stem Coatings
Applying physical vapor deposition (PVD) nano-ceramic thin films to stainless steel stem threads, lowering thread friction coefficient to < 0.08 and enabling hand-lever operation on DN600+ high-pressure valves without gear reducers.
8. Frequently Asked Engineering & Procurement Questions
Direct technical answers to common queries raised by pipeline consulting engineers and procurement managers.
Complementary Industrial Valves & Accessories
Complete your project pipeline requirements with our full line of high-performance check valves, butterfly valves, and control valves.