Specialized Venting, Isolation & Control Series
Direct factory supply of precision-engineered air valves, resilient gate valves, and hydraulic control systems built to international DIN, BS, and ANSI standards.
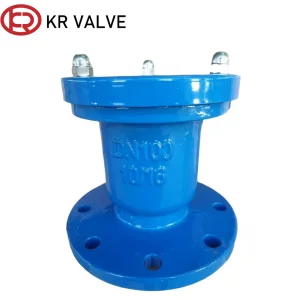
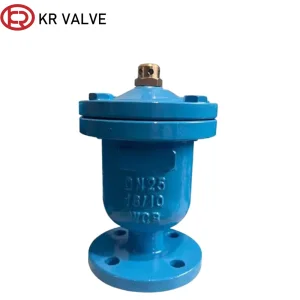
Wholesale Automatic air release valve single port type WCB material PN16 Manufacturer, Factory
View Product Details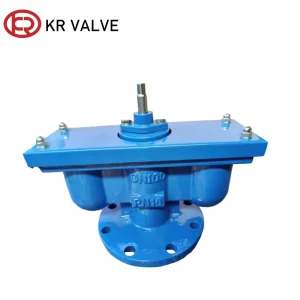
Wholesale Double port air evacuation valve automatic release air Manufacturer, Factory
View Product Details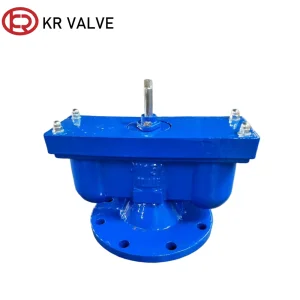
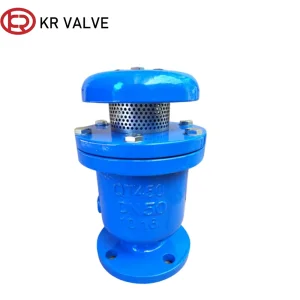
OEM Composite exhaust valve quick exhaust 2-4 inch flange Manufacturer, Factories
View Product Details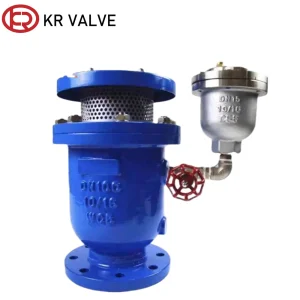
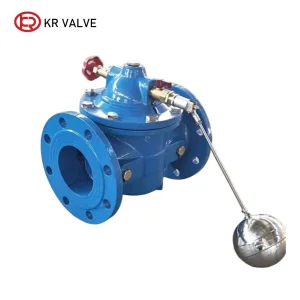
Wholesale Ductile Iron Hydraulic Ball Remote Float Valve - Flange Type 100X Series
View Product Details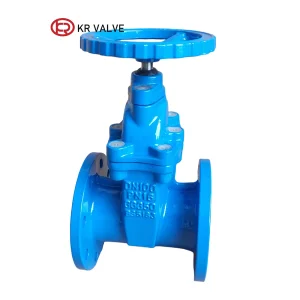
The Global Commercial & Industrial Fluid Dynamics Landscape
Navigating complex infrastructure requirements, severe fluid transients, and corrosive media with specialized valve manufacturing solutions.
In modern mega-scale municipal, chemical, power, and desalination infrastructure, industrial fluid control systems face unprecedented operational stresses. Pipeline networks operate across vast geographical stretches under highly dynamic thermal and static head pressure states. Within these systems, unvented air pockets, hydraulic surge spikes (water hammer), severe cavitation, and chemical degradation represent systemic threats to pipeline integrity and plant operational uptime.
Global EPC contracts, municipal water authorities, and industrial plant owners are increasingly evaluating valve sourcing strategies beyond standard catalogues under the search intent of "Other Suppliers & Factory". This search behavior highlights a critical market demand: the need for reliable, highly specialized OEM/ODM valve manufacturers capable of designing custom flow-control hardware tailored to rigorous fluid dynamics specifications while mitigating total cost of ownership (TCO).
Key market drivers shaping the global valve industry include:
- Infrastructure Modernization & Water Security: Aging municipal supply networks in North America and Western Europe require zero-leakage resilient seated gate valves (DIN F5 / BS5163 standard) and dynamic pressure-reducing control valves to curb non-revenue water (NRW) losses.
- Desalination & Chemical Processing Surge: Seawater reverse osmosis (SWRO) plants and chemical processing facilities demand corrosion-immune split-body full PTFE lined butterfly valves and CF8/CF8M stainless steel check valves capable of resisting aggressive chlorides and acids.
- Hydraulic Transient Mitigation: High-speed compound air release valves (such as the CARX series) are becoming mandatory along water transmission pipelines to prevent catastrophic vacuum collapsing and pressure surge ruptures.
Engineering Architecture & Material Science
An advanced engineering breakdown of air exhaust valves, fluoropolymer sealing, and hydraulic float mechanisms.
Air Release & Vacuum Breaker Valves
Entrained air in pressurized liquid mains causes head losses, flow throttling, and surge destructive energy. Advanced single and double port air evacuation valves solve this via aerodynamic float kinetics.
- CARX High-Speed Release: Dual orifice design allows large-volume air exhaust during line filling and rapid air intake during pipeline draining.
- Anti-Shock Mechanism: Prevents premature float closure under high air discharge velocities up to Mach 0.5.
- Material Specs: Ductile Iron (GGG40/GGG50) or WCB cast steel bodies with 304/316 Stainless Steel internal floats and EPDM soft seats.
Split-Body Full PTFE Lined Valves
For highly abrasive and chemically active fluid transport, standard rubber-lined butterfly valves experience accelerated polymer degradation. Split-body PTFE valves deliver absolute isolation.
- Two-Piece Body Architecture: Simplifies seat replacement and enables uniform compression of the virgin PTFE/PFA lining.
- Full Fluoropolymer Encapsulation: Eliminates direct contact between corrosive media and metal body structures (Ductile Iron GGG40).
- Live-Loaded Shaft Sealing: Belleville spring-washer sets compensate for thermal expansion and contraction cycles.
Hydraulic Remote Control (100X Series)
Pilot-operated remote float control valves regulate fluid levels in storage reservoirs without requiring external electrical power sources, utilizing pipeline hydraulic pressure.
- Diaphragm-Actuated Trim: Nylon-reinforced EPDM diaphragm ensures high-sensitivity opening/closing responsive cycles.
- Cavitation Protection: Engineered needle valve pilot controls closing speed to prevent pressure spikes during shut-off.
- Flange Standards: Compatible with DIN PN10/PN16 and ANSI Class 150/300 raised-face configurations.
Information Gain Insight: Unlike standard off-the-shelf valves, KR Valve's specialized production lines utilize vacuum-tested, high-density PTFE lining (minimum 3mm thickness) and fusion-bonded epoxy coating (FBEC, min 250 microns) certified to DIN 30677-2, preventing pinhole corrosion and micro-delamination under continuous thermal cycling.
| Valve Category | Primary Sealing Material | Design Standard | Nominal Diameter (DN) | Core Application Environment |
|---|---|---|---|---|
| CARX Compound Air Valve | SS304 Float + NBR/EPDM | EN 1074-4 / ANSI C512 | DN25 - DN300 (1" - 12") | Water transmission high-points, pump stations |
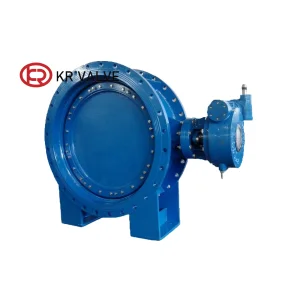
| Split-Body PTFE Butterfly | Virgin PTFE / PFA Liner | API 609 / EN 593 / ISO 5752 | DN50 - DN600 (2" - 24") | Chemical manufacturing, acid pickling, SWRO |
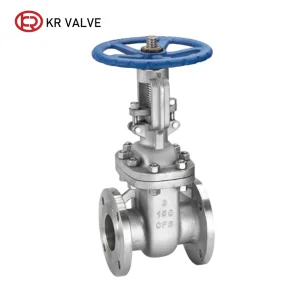
| Resilient Gate Valve (DIN F5) | EPDM Vulcanized Wedge | DIN 3352 F5 / BS5163 | DN40 - DN1200 (1.5" - 48") | Municipal potable water, underground burial |
| Triple Eccentric Hard Seal | Stellite + Stainless Steel | API 609 Cat B / ASME B16.34 | DN80 - DN2000 (3" - 80") | High-temp steam, power plant cooling, refining |
| 100X Remote Float Valve | Reinforced EPDM Diaphragm | CJ/T 219 / JB/T 10674 | DN50 - DN800 (2" - 32") | Elevated water tanks, municipal storage dams |
Localized Application Scenarios & Engineering Cases
Tailored fluid control deployments across severe industrial, municipal, and energy sector environments.
Municipal Water Treatment & Infrastructure
In large-scale municipal water distribution projects across Southeast Asia, Europe, and South America, maintaining zero-leakage isolation and preventing transient pipe bursts is vital.
- DIN F5 Resilient Seated Gate Valves: Installed in underground vault installations. Non-rising stem (NRS) design with EPDM encapsulated ductile iron wedges guarantees bubble-tight shut-off (ISO 5208 Rate A).
- CARX Air Release Valves: Placed at peak elevation contours to automatically purge accumulated air bubbles during operating pressures up to 16 Bar.
Desalination & Chemical Processing Plants
Handling concentrated brine, sodium hypochlorite, and industrial acids requires extreme chemical resistance and resistance to pitting corrosion.
- Split-Body Full PTFE Lined Butterfly Valves: Engineered with SS316 disc cores encapsulated in thick PTFE. Provides seamless flow isolation against aggressive chemical media.
- CF8 Stainless Steel Swing Check Valves: Protect high-pressure SWRO feed pumps against backflow reversal with zero hinge pin degradation.
China Factory Supply Chain Resilience & Efficiency
Leveraging the Tianjin Valve Industrial Cluster to deliver superior quality control, cost efficiency, and rapid export lead times.
Global procurement teams evaluating valve OEM suppliers require more than high technical specs—they require supply chain stability, scalable production volume, and rigorous quality assurance protocols. Operating from Tianjin, China's premier industrial valve manufacturing hub, KR Valve (Tianjin) Co., Ltd. integrates full-chain production capabilities.
Vertically Integrated Quality Control
From sand casting and precision CNC machining to electrostatic epoxy powder coating and pressure testing, every step occurs in-house under strict ISO 9001 quality management systems.
Cost-Efficiency & Scale Economies
By pairing automated foundry processes with centralized raw material purchasing (Ductile Iron, WCB, SS304/316), KR Valve minimizes unit costs while maintaining international standard compliance.
OEM/ODM Contract Customization
Full engineering drawing support for client-branded valve castings, customized face-to-face dimensions (DIN, BS, ANSI, JIS), specialized gear actuators, and export plywood packaging.
Technology Roadmap & Future Engineering Outlook
Pioneering smart IoT fluid integration, zero-emission sealing, and digital twin valve manufacturing.
As industrial automation advances toward Industry 4.0 standards, valve hardware is evolving from passive mechanics into intelligent, sensor-integrated edge nodes. KR Valve's long-term technical roadmap centers on three key innovation pillars:
1. Smart IoT & Actuation
Integrating wireless pressure, acoustic leakage, and position sensors directly into air valve bonnets and hydraulic pilots to provide real-time SCADA telemetry and predictive maintenance alerts.
2. Advanced Elastomer Synthetics
Developing next-generation nano-composite PTFE matrices and peroxide-cured EPDM formulations to expand thermal operating envelopes from -20°C to +200°C without elastomer degradation.
3. CFD & Topological Optimization
Utilizing Computational Fluid Dynamics (CFD) modeling to re-engineer internal valve flow profiles, reducing fluid friction loss coefficients ($\zeta$) by up to 22% for higher energy efficiency.
Localized Support & Compliance Framework
Rigorous international certification, complete documentation, and global technical assistance.
To eliminate compliance risks for international engineering contractors, KR Valve enforces strict adherence to global standard benchmarks:
- Pressure Testing & Inspection: 100% shell hydrostatic test (1.5x PN) and seat tightness test (1.1x PN) in compliance with API 598 and EN 12266-1 prior to dispatch.
- International Approvals: ISO 9001:2015 Quality Management System, ISO 14001 Environmental Management, CE PED 2014/68/EU certification, WRAS potable water approval.
- Comprehensive Documentation Package: Every shipment includes EN 10204 3.1 Material Test Certificates, Non-Destructive Examination (NDE/NDT) reports, coating thickness verification, and hydro-test charts.
Frequently Asked Technical Questions
Expert responses to critical valve selection, installation, and procurement inquiries.
Specialized PTFE Lined, Check & Gate Series
High-durability butterfly valves, CF8 check valves, and triple-eccentric pneumatic configurations direct from factory stock.
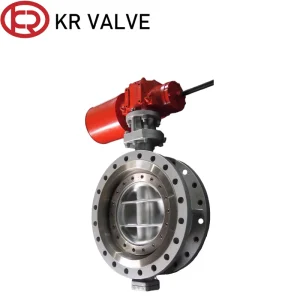
Wholesale Single acting pneumatic three eccentric butterfly valve hard seal 150LB Manufacturers, Factories
View Product Details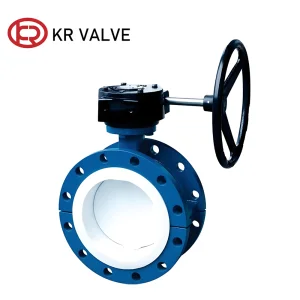
Wholesale China Ductile Iron Split Body Full PTFE Butterfly Valve Suppliers | Factory Direct Sales
View Product Details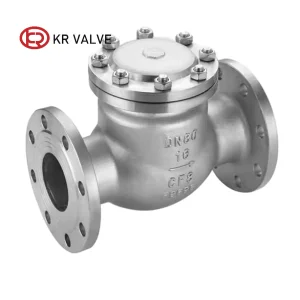
Custom Ductile iron material split body full PTFE butterfly valve Manufacturers, Manufacturer
View Product Details
Custom Double Port Air Evacuation Valve - Automatic Release Air | China Suppliers & Factory
View Product Details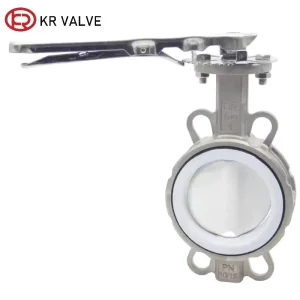
OEM China PTFE Lined Wafer Butterfly Valve with SS Body - Top Suppliers and Factory Solutions
View Product Details