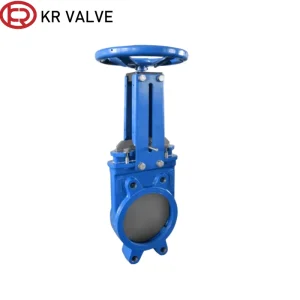
Explore our top-tier catalog of precision-engineered automated, knife gate, butterfly, and check valves designed for municipal water networks, slurry treatment, and high-pressure fluid lines.
The global industrial valve market is undergoing a seismic paradigm shift. Traditional manual isolation valves are rapidly giving way to intelligent, automated gate valve assemblies integrated with Industrial Internet of Things (IIoT) sensors, smart pneumatic actuators, and multi-turn electric drive units. Driven by global initiatives for process automation, water infrastructure modernization, and decarbonization in energy sectors, the demand for precision-engineered custom automated gate valves has reached unprecedented heights.
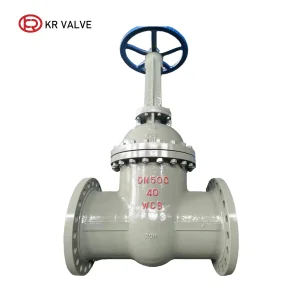
Automated gate valves serve as critical bi-directional isolation devices in high-pressure, high-temperature, and corrosive pipeline networks. Unlike throttling valves, a gate valve provides a straight-through full-bore fluid pathway, minimizing pressure drop (${\Delta}P$) and turbulence across the valve seat. When retrofitted or natively engineered with electric (e.g., AUMA, Rotork compliant), pneumatic (double-acting or spring-return), or electro-hydraulic actuators, these assemblies offer millisecond signal responsiveness, remote telemetry feedback, and SIL-3 safety trip execution.
Technical Reality Check: In modern smart city water distribution and chemical plant engineering, manual valve operation introduces human error, operational latency, and unacceptable safety risks. Custom automated gate valves engineered by accredited manufacturers eliminate mechanical backlash, incorporate real-time torque limiters, and allow centralized SCADA systems to monitor valve disc position down to 0.1% accuracy margins.
Off-the-shelf valves frequently fail when subjected to aggressive abrasive slurries, cryogenic temperatures, or severe thermal cycling. Premier Chinese factories specialize in tailored engineering solutions across all critical valve components.
Body and bonnet materials cast or forged according to precise process fluids: WCB (ASTM A216), Ductile Iron GGG40/50 (EN-GJS-400-15), Stainless Steel SS304/SS316L (ASTM A351 CF8/CF8M), Super Duplex (2205/2507), and Hastelloy C276 for extreme chemical resistance.
Resilient EPDM/NBR seats for zero-leakage municipal water networks, full PTFE/PFA lining for acid transport, or Stellite No. 6 hardfacing metal-to-metal seating for abrasive mining slurries operating at temperatures up to 550°C.
Direct ISO 5211 top-flange mounting interfacing with 4-20mA HART, Modbus RS485, Profibus DP, or Ethernet/IP protocols. Equipped with manual handwheel override, explosion-proof ATEX/IECEx enclosures, and emergency fail-safe spring returns.
Stem Sealing and Fugitive Emission Control
Environmental regulations such as ISO 15848-1 and EPA Method 21 demand stringent control over stem seal packing leakage. Custom automated gate valve suppliers incorporate live-loaded graphite packing rings, dual O-ring stem seals, and precision-ground 13Cr or SS316 stems with surface finish Ra < 0.4 µm. This reduces friction torque, lengthens packing lifespan, and ensures full compliance with international environmental standards.
Over the past two decades, China has evolved from a high-volume hardware producer into the world's leading hub for high-precision, heavy-duty industrial valve manufacturing. Key industrial clusters in Tianjin, Zhejiang (Wenzhou/Lishui), and Jiangsu have formed integrated valve production ecosystems that offer global EPC contractors and distributors unmatched competitive advantages.
Chinese valve manufacturing hubs feature vertically integrated supply chains—from automated shell molding foundries to multi-axis CNC machining centers. This minimizes raw material transport lag and ensures strict dimensional tolerances matching ANSI, DIN, BS, and JIS standards.
Leading suppliers implement 100% pressure testing protocols conforming to API 598 and EN 12266-1. Every automated gate valve undergoes shell testing, high-pressure closure testing, and low-pressure pneumatic seat testing before assembly packaging.
Through streamlined production, localized component sourcing, and optimized labor efficiency, Chinese automated gate valve factories deliver savings of 25% to 45% on Total Cost of Ownership (TCO) compared to Western European counterparts without compromising quality.
Automated gate valves are deployed across diverse operating environments. Specific media, pressure profiles, and operational frequencies dictate unique engineering configurations.
| Industrial Sector | Primary Valve Type Spec | Typical Media & Pressure | Engineering Customization Focus |
|---|---|---|---|
| Municipal Water & Wastewater | Resilient Seated Gate Valve (BS5163 / DIN F4/F5) | Raw water, treated effluent, 10–25 bar | EPDM fully encapsulated wedge, WRAS approved non-toxic epoxy coating (250µm DFT), IP68 submersible electric actuator. |
| Mining & Mineral Processing | Pneumatic Knife Gate Valve (Lug / Wafer Type) | Abrasive copper/iron tailings, slurry, 6–16 bar | Replaceable polyurethane or Ni-Hard liners, SS316L knife blade with chrome plating, bi-directional bubble-tight shut-off. |
| Oil & Gas Midstream Pipeline | High Pressure Cast Steel Gate Valve (Z41H / API 6D) | Crude oil, natural gas, Class 150 to Class 1500 | Flexible wedge design, Stellite hardfaced seats, fire-safe certified to API 607, electro-hydraulic actuator fail-safe system. |
| Chemical & Petrochemical Plants | PTFE Lined or Stainless Steel Floating/Gate Valve | Acids, alkalis, solvent streams, PN16–PN64 | Full PTFE/PFA corrosion barrier, bellows seal design for zero fugitive emissions, ATEX explosion-proof electric drive. |
| Thermal Power & District Heating | Big Size Metal-to-Metal Sluice Valve (DN500+) | Superheated steam, high temp boiler water | Pressure seal bonnet design, WC6/WC9 alloy steel construction, high-torque motorized gearbox integration. |
For overseas procurement managers, EPC contractors, and global distributors, purchasing custom automated gate valves from China requires a balance between unit acquisition cost and long-term operating reliability. Implementing a structured supplier evaluation framework mitigates supply chain risks.
Ensure the supplier holds verified certifications: ISO 9001:2015 Quality Management, CE PED (Pressure Equipment Directive 2014/68/EU), API 6D / API 600 certificates, and WRAS/DVGW drinking water approvals where applicable.
Verify that top flanges strictly conform to ISO 5211 dimensions. Standardized stem drives allow smooth field replacement of actuators (AUMA, Rotork, Festo, SMC) without custom machining on job sites.
Demand EN 10204 3.1 chemical and mechanical material certification for all pressure-retaining bodies, stems, and wedges. Third-party inspections (SGS, TUV, BV) provide independent verification prior to sea freight shipment.
Procurement Pro-Tip: Always request factory-installed wiring diagrams, calibration test certificates for automated positioners, and complete operation & maintenance manuals (O&M) in English alongside shipment documentation to avoid installation delays during plant commissioning.
Clear, direct engineering answers addressing common technical queries and supply chain logistics for custom automated gate valves.
Discover our comprehensive collection of forged steel check valves, SS304 ball valves, resilient gate valves, and specialized pressure control systems manufactured for export worldwide.