Industrial Electric & Mechanical Valves for Water Infrastructure
Explore our top-tier OEM industrial valves engineered for municipal water supply, wastewater plants, and automated industrial processing lines.
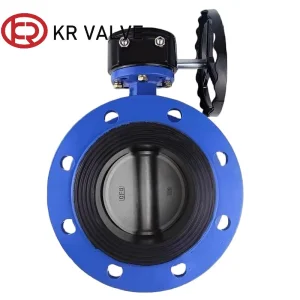
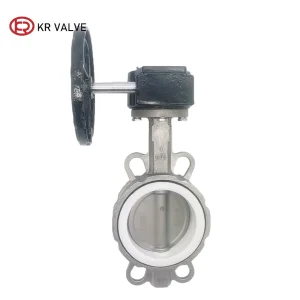
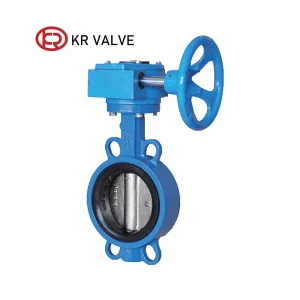
The Automation Paradigm: OEM Electric Valves in Modern Water Factories
As global industrial water infrastructure undergoes rapid digital transformation under Industry 4.0 paradigms, the transition from manual multi-turn handwheel isolation valves to intelligent Motor-Operated Valves (MOVs) has become a technical prerequisite for municipal and commercial facilities.
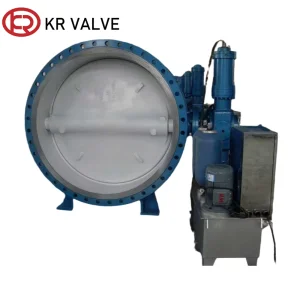
In modern water treatment plants, desalination facilities, and large-scale industrial manufacturing factories, fluid management demands unprecedented levels of precision, speed, and remote control integration. The modern OEM electric valve for water factories represents the convergence of high-durability mechanical engineering and state-of-the-art electronic actuation. Integrating SCADA (Supervisory Control and Data Acquisition) protocols directly into local terminal units allows water management engineers to monitor hydraulic pressure spikes, modulate volumetric flow rates, and execute fail-safe emergency cut-offs within milliseconds.
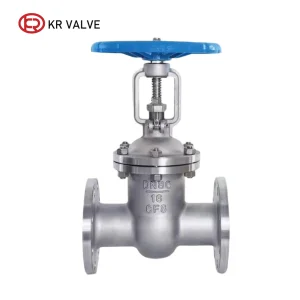
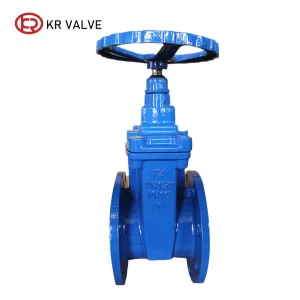
Historically, water infrastructure relied heavily on manual gate valves (such as legacy DIN F4/F5 or BS5163 non-rising stem designs) or basic pneumatic assemblies. However, compressed air networks in expansive water treatment factories present high energy losses, maintenance overheads, and pneumatic line freeze risks. Electric actuators eliminate the need for centralized air compressors, offering direct electrical-to-mechanical energy conversion with operating thermal efficiency ratings exceeding 90%.
Engineering Architecture & Actuator Kinematics
Deconstructing the internal mechanics, elastomer seating technologies, motor drive electronics, and ISO 5211 mounting interfaces of high-performance electric water valves.
Intelligent Actuator Controls
Modern electric actuators feature brushless DC or synchronous AC motors paired with planetary gear reductions, delivering non-penetrating magnetic setup, multi-bus communication, and high break-away torque.
- Modulating 4-20mA & 0-10V analog input
- Modbus RTU, Profibus-DP, HART protocols
- Supercapacitor fail-safe return options
Valve Body Geometry
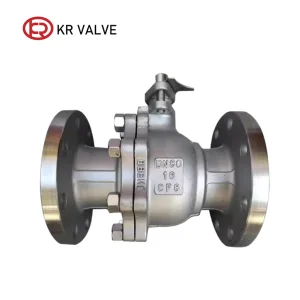
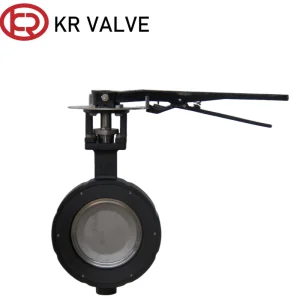
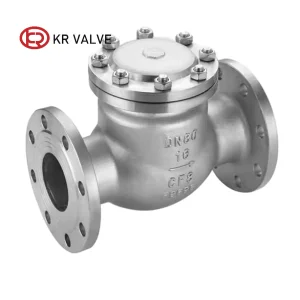
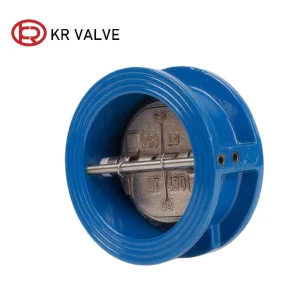
Selecting the optimal valve body configuration—concentric, double eccentric, or triple offset butterfly valves, resilient seated gate valves, or non-slam dual plate check valves—directly governs hydraulic Cv factors.
- Full-bore low hydraulic friction designs
- Bi-directional zero-leakage seating
- ISO 5211 direct-mount actuator flanges
Advanced Elastomers & Coatings
Protecting structural iron against cavitation, micro-cracking, and chemical disinfection agents requires electrostatic fusion-bonded epoxy (FBE) barrier coatings and drinking-water-certified seats.
- WRAS / DVGW / NSF-61 EPDM & NBR liners
- FBE powder coating > 250 µm thickness
- CF8 / CF8M stainless steel disc cladding
Technical Specification Matrix: Electric Water Valve Series
| Valve Type | Body Material | Nominal Size (DN) | Pressure Rating | Actuator Type | Ingress Protection | Standard Compliance |
|---|---|---|---|---|---|---|
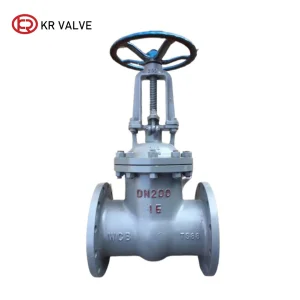
| Resilient Seated Gate Valve | Ductile Iron GGG40 / GGG50 | DN50 - DN1200 (2" - 48") | PN10 / PN16 / Class 150 | Multi-Turn Electric (380V/220V) | IP67 / IP68 (Submersible) | DIN 3352 F4/F5, BS 5163, AWWA C509 |
| Concentric Butterfly Valve | Ductile Iron / CF8 Stainless | DN40 - DN600 (1.5" - 24") | PN6 / PN10 / PN16 | Quarter-Turn Modulating MOV | IP67 NEMA 4/4X | API 609, ISO 5752, EN 593 |
| Double Eccentric Butterfly Valve | Ductile Iron / Cast Steel WCB | DN200 - DN3000 (8" - 120") | PN10 / PN16 / PN25 | Quarter-Turn Heavy Duty Gearbox | IP68 Waterproof Actuator | BS EN 593, DIN 3202 F4 |
| Dual Plate Wafer Check Valve | Ductile Iron / Stainless Steel | DN50 - DN800 (2" - 32") | PN10 / PN16 / Class 150/300 | Spring Return (Mechanical) | N/A (Inline Self-Operating) | API 594, BS 5153, EN 12334 |
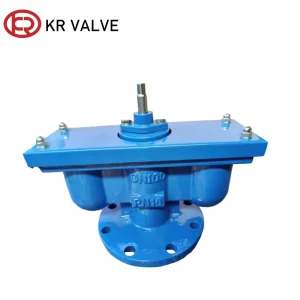
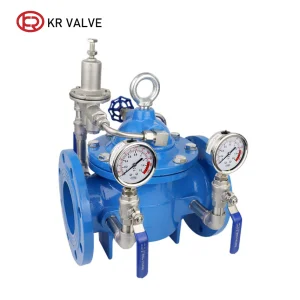
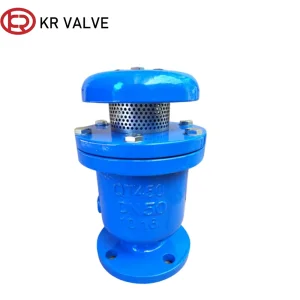
| Hydraulic 200X Pressure Valve | Ductile Iron QT450-10 | DN50 - DN600 (2" - 24") | PN10 / PN16 / PN25 | Electric Solenoid Pilot Control | IP65 / IP67 Solenoid Enclosures | CJ/T 219, JB/T 10674 |
China OEM Supply Chain Resilience: Tianjin Valve Manufacturing Cluster
How end-to-end integration—from resin-sand foundry casting to precision CNC machining and automated testing—delivers global cost-to-performance superiority.
Vertical Integration & Manufacturing Scale
Global procurement teams in the water utility sector encounter significant challenges regarding supply lead times, dimensional inconsistency, and escalating material costs. Tianjin, China, stands as one of the world's most sophisticated manufacturing hubs for industrial fluid control equipment. By establishing unified supply chains spanning over 30 specialized manufacturing facilities, premier China valve factories offer unmatched operational scalability.
The manufacturing lifecycle of an OEM electric valve for water factories begins in state-of-the-art foundries using spectrographic resin-sand casting methods. This ensures that cast iron (GG25) and ductile iron (GGG40 / QT450-10) bodies meet precise metallurgical densities without micro-porosity or internal inclusion flaws. Computerized CNC horizontal machining centers then mill face-to-face dimensions, stem guide keyways, and ISO 5211 actuator mounting pads to tolerances within ±0.01mm.
Furthermore, automated electrostatic powder coating lines apply drinking-water approved epoxy resin under strictly controlled thermal conditions. This guarantees complete coating uniformity exceeding 250 micrometers, providing long-term resistance against soil galvanic corrosion and chemical tuberculation in underground municipal water pipelines.
100% Pressure Hydrostatic Inspection
Every single valve produced undergoes rigorous shell testing at 1.5x nominal pressure and seat leak testing at 1.1x nominal pressure in strict accordance with ISO 5208, EN 12266-1, and API 598 before final packaging.
Custom OEM Branding & Engineering
We provide full white-label OEM support, offering custom stem extensions, customized flange drilling standards (ANSI, DIN, BS, JIS), custom actuator voltage inputs, and customized private brand branding.