Primary Industrial Valve Solutions (Top 8 Portfolio)
Explore our high-performance OEM gate, sluice, and butterfly valve systems designed for extreme pressure rating, aggressive fluid media, and high-cycle longevity.
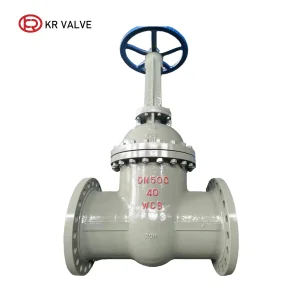
Evolution & Macro Trends in Stainless Steel Gate Manufacturing
The global industrial flow control sector is undergoing a monumental paradigm shift. Driven by stricter environmental regulations, zero-leakage mandates in chemical processing, and the expansion of seawater desalination infrastructure, modern engineering projects are increasingly phasing out legacy cast iron and carbon steel valves in favor of high-grade austenite and duplex stainless steel gate valves.
Material Science Advancements
The market is shifting rapidly from standard CF8 (SS304) to super-austenitic (such as 6% Mo alloys) and Duplex/Super Duplex stainless steels (2205 / 2507). These materials eliminate pitting corrosion and stress corrosion cracking (SCC) in chloride-rich environments like desalination plants and offshore platforms.
Precision OEM Digitalization
Top-tier OEM suppliers now integrate 3D CAD parametric modeling, Computational Fluid Dynamics (CFD) simulation for low fluid resistance, and Finite Element Analysis (FEA) to verify wedge structural integrity under PN64 to PN160 pressures before physical pouring occurs.
Strict Compliance & ESG
Global buyers require ISO 14001 certified manufacturing alongside ISO 15848-1 low-fugitive emission stem packing certifications. OEMs must deliver full material traceability back to raw ingot heats via EN 10204 3.1 chemical & mechanical mill test reports (MTRs).
Decoding Global Sourcing Requirements for OEM Gate Valves
When EPC contractors, project engineers, and industrial procurement managers search for "OEM Stainless Steel Gate Suppliers & Factories", their search intent extends far beyond standard pricing. They seek verified technical competence, precise dimensional interchangeability, custom flange drilling compliance, and rigorous quality control protocols.
Primary Sourcing Drivers for EPCs
- Exact Face-to-Face Standard Matching: Strict adherence to ASME B16.10, DIN 3202 (F4/F5), or BS 5163 dimensions to ensure plug-and-play installation without piping stress.
- Zero-Leakage Sealing Options: Availability of both soft-seated (EPDM/PTFE) for bubble-tight low-temp service and hard metal-to-metal (Stellite hardfacing) for high-pressure/temp fluids.
- Actuation & Automation Compatibility: Standardized ISO 5211 top flange mounting pads for effortless mounting of electric multi-turn, pneumatic, or hydraulic actuators.
- NACE MR0175 / ISO 15156 Compliance: Resistance to sulfide stress cracking in sour gas and crude oil environments.
OEM Partner Evaluation Matrix
- In-House Metallurgy & Foundry Testing: Spectrometer chemical composition analysis, Radiographic (RT), Ultrasonic (UT), and Magnetic/Penetrant (PT) flaw detection.
- Custom Wedge & Stem Designs: Flexibility to manufacture Flexible Wedge, Solid Wedge, Split Wedge, or Knife Gate configurations based on medium viscosity.
- Fast-Track OEM Tooling & Prototyping: Ability to convert customer CAD models into investment casting molds within accelerated 14-day timelines.
- Comprehensive Export Logistics: Heavy-duty export-grade plywood case packaging, anti-corrosion VCI wrapping, and multi-country trade documentation support.
Metallurgical Specifications & Material Selection Matrix
Selecting the correct stainless steel grade is paramount to avoiding catastrophic failure in industrial flow control. The table below outlines our OEM manufacturing options across standard and exotic alloy grades.
| Alloy Grade | UNS / Cast Equivalent | Chemical Composition Key Elements | Corrosion & Temperature Limits | Recommended Industrial Applications |
|---|---|---|---|---|
| SS304 / CF8 | UNS J92600 / 1.4308 | 18-20% Cr, 8-11% Ni | -196°C to +425°C / Moderate oxidation resistance | Potable water, HVAC, food processing, light industrial lines |
| SS316 / CF8M | UNS J92900 / 1.4408 | 16-18% Cr, 10-14% Ni, 2-3% Mo | -196°C to +600°C / Superior chloride pitting resistance | Seawater treatment, chemical lines, pharmaceutical, paper pulp |
| SS316L / CF3M | UNS J92800 / 1.4404 | Low Carbon (<0.03%), Mo 2-3% | Prevents intergranular corrosion post-welding | High-purity chemical plants, acid handling, cryogenic lines |
| Duplex 2205 | UNS J92205 / CD3MN (1.4462) | 22% Cr, 5% Ni, 3% Mo, 0.18% N | High yield strength (2x SS316), PREN > 34 | Desalination high-pressure RO skids, offshore oil & gas, mining |
| Super Duplex 2507 | UNS J93404 / CE3MN (1.4410) | 25% Cr, 7% Ni, 4% Mo, 0.27% N | Extreme pitting resistance, PREN > 42 | Marine splash zones, concentrated acid transport, subsea valves |
Macro Industry Solutions & Heavy-Duty Application Scenarios
Our OEM stainless steel gate valves and sluice gates are field-proven across critical infrastructure sectors worldwide. Engineered to handle extreme thermal cycles, high differential pressures, and slurry-laden fluids, they deliver unmatched operational security.
1. Desalination & Marine Infrastructure
In Seawater Reverse Osmosis (SWRO) facilities, high salinity combined with 70+ bar operating pressures degrades standard materials within months. Our custom Duplex 2205 gate valves with micro-polished disc faces ensure total isolation on pump discharge lines without crevice corrosion.
2. Petrochemical & Refining Refineries
Handling volatile hydrocarbons and aggressive sulfur compounds requires API 600 compliant CF8M gate valves equipped with flexible wedges and graphite packing rings. Designed to withstand fire test conditions according to API 607, protecting refinery assets against toxic leakage.
3. Municipal Wastewater & Drainage
Large-scale municipal storm treatment plants demand heavy-duty stainless steel penstock sluice gates (up to DN3000). Designed with ultra-low friction self-lubricating HDPE seals, these gates handle high head pressure while preventing debris binding.
Quality Assurance, NDT Testing & International Compliance
As an established OEM manufacturer, quality is non-negotiable. Every individual valve manufactured in our factory undergoes rigorous 100% hydrostatic and pneumatic pressure testing prior to dispatch.
Shell & Seat Hydro Test
Tested at 1.5x PN rating for shell pressure and 1.1x PN rating for high-pressure closure per API 598 or EN 12266-1 standard.
PMI Material Verification
X-ray Fluorescence Positive Material Identification (PMI) conducted on body castings and stem stock to prevent alloy mix-ups.
Wall Thickness Precision
Ultrasonic thickness testing (UT) guarantees cast wall dimensions exceed API 600 minimum thickness thresholds for ultimate safety margin.
Low Fugitive Emissions
Tested according to ISO 15848-1 AH Class with helium leak detection to guarantee environmental containment in volatile chemical lines.
Technology Roadmap: Next-Generation OEM Stainless Steel Gate Valves
Looking ahead, our engineering R&D team is advancing smart valve diagnostic capabilities and novel surface treatment technologies to maximize client ROI and operational uptime.
1. Smart Sensor Integration & Predictive Maintenance
Integrating micro-embedded strain gauges and acoustic emission sensors within the gate stem assembly. These sensors continuously monitor stem torque, cycle counts, and seat wear in real-time, transmitting diagnostic data via Modbus or WirelessHART directly to SCADA control rooms to prevent unexpected downtime.
2. Advanced Surface Coatings & Laser Cladding
To extend valve seal life in abrasive mining slurries, we utilize automated laser cladding systems to apply Stellite 6, Tungsten Carbide, or Nickel-Chromium overlays on stainless sealing faces. This achieves hardness exceeding HRC 60 while preserving the ductility of the underlying stainless body.
Frequently Asked Questions (Engineering & Procurement FAQ)
Direct responses to critical technical queries raised by global procurement personnel and valve engineering consultants.
Secondary Flow Control Portfolio (Bottom 8 Products)
Review additional OEM product configurations including hydraulic butterfly valves, stainless steel check valves, and specialty stem gate valves engineered for global supply chains.