Industrial Flow Control & Valve Solutions
High-performance flow isolation and non-return valves manufactured to ANSI, DIN, and BS international engineering standards.
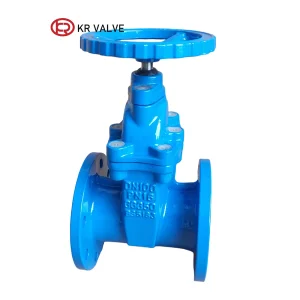
Custom Bronze Seat Gate Sluice Valves: Metallurgy & Tribological Superiority
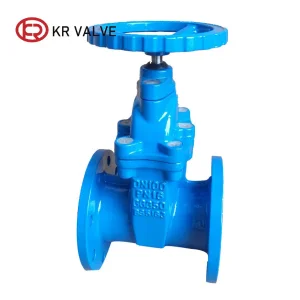
In high-pressure municipal water transmission, raw sewage handling, and coastal desalination applications, standard soft-seated gate valves often succumb to elastomer degradation, wire-drawing erosion, and permanent deformation. Custom bronze seat gate sluice valves engineered by tier-1 China foundries provide the ultimate metal-to-metal seating interface required for zero-leakage reliability over multi-decade lifecycles.
By press-fitting, threaded-locking, or micro-welding high-leaded bronze (ASTM B62 / C83600), aluminum bronze (ASTM B148 C95800), or manganese bronze (ASTM B584 C86300) seat rings directly into high-tensile Ductile Iron (ASTM A536 65-45-12 / GGG40/GGG50) or Cast Steel (WCB) bodies, engineering teams achieve an optimized tribological pairing. The bronze matrix possesses self-lubricating properties, reducing operating torque while demonstrating exceptional resistance to biofouling, dezincification, and cavitation pitting.
Why Metal-Seated Bronze Trim Dominates Severe Duty
- Bi-Metallic Wear Compatibility: Differential hardness ratios between bronze wedge rings and stainless steel stem components prevent galling under high differential pressures (ΔP up to 25 bar).
- Thermal Stability Range: Operates continuously from -20°C to +200°C without elastomer hardening or thermal setting failures common in soft-seated valves.
- Particulate Indentation Resilience: Suspended solids, sand, and tuberculation scale are crushed or wiped clear across the precision-lapped bronze seating surfaces without tearing seal geometry.
Global Enterprise Procurement Demand & Regional Standards
Global infrastructure investments demand compliance with varied international standards. OEM & ODM suppliers must align metallurgy, pressure ratings, and face-to-face dimensions to project specifications.
North America (AWWA C500 & C515)
EPC contractors require heavy-pattern AWWA C500 metal-seated gate valves featuring bronze trim (B62/B584) with non-rising stems (NRS) or outside screw & yoke (OS&Y). Procurement focus centers on 100% domestic testing compliance, ANSI B16.1 Class 125/250 flanging, and NSF/ANSI 61 lead-free bronze certifications.
Europe & Middle East (DIN 3352 / BS 5163)
Driven by massive municipal water grid renovations and SWRO desalination initiatives. Requirements focus on DIN 3352 Part 2 metal-seated sluice valves with EN 1092-2 PN10/PN16/PN25 flanges, DIN F4/F5 face-to-face lengths, and Nickel Aluminum Bronze (C95800) seats to withstand hypersaline sea water intake.
Asia-Pacific & LatAm (Sewerage & Hydro)
Rapid urban sprawl requires cost-optimized, large-diameter sluice gates (DN500 to DN2400). Suppliers are evaluated on foundry melting capacity, sand casting integrity, hydraulic torque testing under full flow, and customized stem extensions for deep-buried pit applications.
Macro-Industry Solutions & Application Scenarios
Deploying custom bronze-seated sluice technology across mission-critical fluid distribution infrastructure.
1. Municipal Raw Water Pumping & Treatment Stations
Raw river water carries abrasive silt, gravel, and organic debris. Standard soft seals cut and fail within months. Custom bronze seat sluice valves utilize a solid wedge design lined with high-hardness manganese bronze ring inserts (HB > 150). When closing against high velocity heads, the bronze seat scours particle buildup while forming a bubble-tight seal under high static hydrostatic pressures.
2. Seawater Desalination (SWRO) & Coastal Power Intakes
Marine environments rapidly attack carbon steels and standard brass trim through galvanic corrosion and chloride pitting. China's top tier factories manufacture gate sluice valves featuring Nickel-Aluminum Bronze (NAB ASTM B148 C95800) seats paired with Duplex Stainless Steel (UNS S31803) stems. This metallurgy eliminates crevice corrosion and cavitation erosion during continuous 24/7 sea water filtration cycles.
3. Hydroelectric Dam Penstocks & Spillway Control
High-head dams generate massive hydraulic thrust load. Custom bronze sluice gate assemblies incorporate bronze guide shoes, bronze stem nuts, and body seat rings engineered to handle extreme lateral forces during mid-stroke throttling or emergency shutoff without chatter, vibration, or body distortion.
4. Industrial Wastewater & Slurry Digesters
Chemical processing effluents and municipal digestate lines require robust metal-to-metal isolation. Bronze-seated gate valves provide immunity to chemical breakdown, swelling, or embrittlement caused by ambient hydrocarbons, industrial solvents, or bio-methane gas byproducts in anaerobic digestor lines.
Technical Roadmap & Future Outlook
How modern Chinese valve factories combine advanced foundry metallurgy with automated CNC precision manufacturing to redefine custom valve output.
Automated dual-disc planetary lapping machines achieve mirror-like seat tightness meeting API 598 zero leakage standard.
Direct-reading optical emission spectrometers verify exact Cu-Al-Fe-Ni elemental ratios before pouring every bronze heat.
Heavy manufacturing bay capabilities for massive municipal and dam-penstock custom sluice valve fabrications.
Next-Gen Technology Roadmap (2026-2030)
The evolution of custom bronze seat gate sluice valves centers around three engineering vectors:
1. Automated Laser Cladding Seats
Replacing mechanical threaded rings with laser-deposited cobalt-bronze or nickel-bronze overlays directly fused to ductile iron castings, eliminating body-seat crevice leak paths completely.
2. Smart Actuation & IoT Torque Telemetry
Integration of non-intrusive smart multi-turn actuators with embedded load cells to monitor seat wear, torque spikes, and predictive maintenance schedules over SCADA networks.
3. FEA Fluid-Structure Optimization
Finite Element Analysis (FEA) and Computational Fluid Dynamics (CFD) modeling to slim body casting weight by 15% while raising pressure rating bounds to PN40 and ANSI Class 300.
Seating Technology Comparative Analysis Matrix
Compare custom bronze seat sluice valves against soft-seated gate valves and stainless steel trim variants to select the ideal trim specification for your infrastructure pipeline project.
| Performance / Feature Parameter | Custom Bronze Seat Gate Sluice (B62 / C95800) | Resilient Soft Seat Gate Valve (EPDM / NBR) | Stainless Steel Metal Seat (SS304 / SS316) |
|---|---|---|---|
| Primary Seating Interface | Bronze-to-Bronze / Bronze-to-SS Metal Contact | Elastomer Encapsulated Ductile Iron Wedge | Stainless Steel-to-Stainless Steel Metal Contact |
| Operating Temperature Range | -20°C to +200°C (-4°F to 392°F) | -10°C to +70°C (14°F to 158°F) | -40°C to +400°C (-40°F to 752°F) |
| Slurry & Abrasive Sand Handling | Excellent (Crushes solids, self-wiping) | Poor (Particulates tear rubber membrane) | Moderate (Risk of galling under friction) |
| Biofouling & Marine Resistance | Exceptional (Natural copper biocide effect) | Moderate (Algae & biofilm buildup on rubber) | High (Requires high alloy grades like SS316) |
| Service Life Expectancy | 30 - 50+ Years (In-situ lap repairable) | 10 - 15 Years (Requires full wedge replacement) | 25 - 40 Years |
| Closing Torque Requirement | Moderate (Self-lubricating bronze properties) | Low (Elastic deformation soft sealing) | High (High friction coefficient between steel surfaces) |
| Standards Compliance | AWWA C500, DIN 3352, BS 5163, ISO 5996 | AWWA C509 / C515, EN 1171 | API 600, BS 1414, ISO 10434 |
Rigorous Factory Testing & Global Compliance
Top China custom gate valve suppliers adhere to zero-compromise quality assurance frameworks. Every cast body undergoes chemical analysis via X-ray fluorescence (XRF) and mechanical testing (Tensile, Yield, Elongation) prior to precision machining.
100% Hydrostatic & Shell Pressure Testing
Tested in accordance with ISO 5208 Rate A / API 598. Shell tests executed at 1.5x PN rating; high-pressure seat closure tests held at 1.1x PN rating with bi-directional drop-tight verification.
Material Traceability & EN 10204 3.1 Certification
Complete physical and chemical test mill reports provided for body iron, stem stainless steel, and cast bronze seat batch heats for total project auditing peace of mind.
Potable Water & Environmental Safety
Fusion-bonded epoxy (FBE) internal and external coatings compliant with WRAS, GSK, and ANSI/NSF 61 certifications, guaranteeing non-toxic drinking water safety.
Global Engineering & OEM Partnership Capabilities
From custom face-to-face dimensions to non-standard stem nut threading and gear operator retrofits, China's leading valve manufacturing hubs provide end-to-end custom engineering support for international buyers:
- Custom CAD & 3D STEP File Generation: Instant engineering integration into plant BIM or GIS pipeline models within 24 hours of technical query.
- Third-Party Inspection Coordination: Full support for Lloyd's Register, SGS, TÜV, and BV witness testing protocols at the factory floor.
- Export Packaging & Seaworthy Protection: Heavy-duty wooden crating with vapor-corrosion inhibitor (VCI) shrink wrapping to protect polished bronze seats during long maritime shipments.
Frequently Asked Questions by Valve Engineers & EPC Buyers
Answers to common technical inquiries regarding design, material selection, procurement, and maintenance of custom bronze-seated sluice gate valves.
What specific bronze alloy grades are recommended for custom gate sluice valve seats?
How do factories install bronze seat rings into iron gate valve bodies?
Is galvanic corrosion a risk between the cast iron body and the bronze seat rings?
What is the difference between AWWA C500 metal-seated gate valves and AWWA C515 valves?
Can custom bronze seat gate sluice valves be repaired or refaced in the field?
What custom OEM choices are available for stem materials and gear operators?
Complete Pipeline Accessories & Specialty Control Valves
Explore our comprehensive catalog of strainers, hydraulic control valves, and specialty check valves engineered for global waterwork programs.