Explore our top-tier manufacturing pipeline including single-acting pneumatic valves, air release valves, strainers, and specialized butterfly/check valve units.
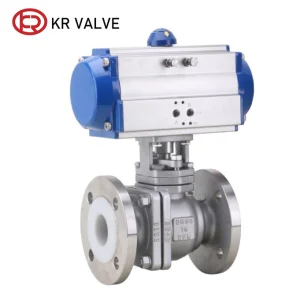
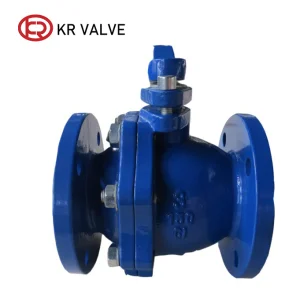
In modern fluid dynamics and industrial process piping, the Floater Ball Valve (Floating Ball Valve) represents the fundamental cornerstone of reliable shut-off functionality. Unlike trunnion-mounted valve architectures where the ball is anchored by upper and lower shafts, a floater ball valve features an unconstrained sphere suspended between two resilient polymer or elastomeric seat rings.
The operational mechanics of floating ball valves rely on fluid pressure differential. When line pressure acts upon the upstream face of the unanchored sphere, the ball physically shifts micro-millimeters downstream against the downstream seat ring. This force compresses the resilient seating matrix (such as RPTFE, PEEK, or Devlon V-API), generating a tight bubble-tight sealing interface.
Thermal expansion of trapped liquid within the valve cavity can cause dangerous pressure spikes. Advanced wholesale floater ball valves engineered at our facility integrate automatic body cavity pressure relief mechanisms. When cavity pressure exceeds upstream pipeline pressure by a predetermined margin, the upstream seat deflects micro-elastically, discharging excess pressure back into the line.
Our ball valve stems feature an internally inserted shoulder design that makes blowout physically impossible under pipeline pressure. Multiple live-loaded Belleville spring washers maintain constant axial load on the V-ring packing stem seals, ensuring continuous sealing under thermal cycling and heavy dynamic operating frequency.
Material Specification Matrix for High-Performance Floater Valves
| Valve Component | Standard Configuration | Corrosive / Chemical Service | High-Temperature / High-Pressure |
|---|---|---|---|
| Body Material | ASTM A216 WCB / A105 Carbon Steel | ASTM A351 CF8M / CF3M (316/316L SS) | ASTM A995 Duplex 2205 / Super Duplex 2507 |
| Floating Ball | SS304 / SS316 Solid Forged Sphere | SS316L + Electro-less Nickel Plating (ENP) | Inconel 625 Clad / Stellite Hardfacing |
| Seat Insert | Virgin PTFE / Reinforced RPTFE (15% Glass) | Modified TFM 1600 / Carbon-Filled PTFE | PEEK / Devlon V-API / Metal-to-Metal Seat |
| Stem Sealing | Flexible Graphite + PTFE V-Ring | Kalrez O-Rings + Graphite Seal Rings | Inconel Live-Loaded Graphite Packing |
The international demand for industrial valve infrastructure is undergoing a massive shift. Driven by energy transitions, industrial automation, and expanding municipal water grids, EPC contractors and procurement officers are prioritizing long-term operational efficiency over initial acquisition costs.
Global buyers are moving away from multi-tiered intermediary supply chains toward verified direct-manufacturer partnerships. Direct factory cooperation guarantees traceable material test reports (MTRs to EN 10204 3.1), standardized quality control inspections, and customized dimensional adaptations (ANSI B16.10, DIN 3202, ISO 5752).
With stringently enforced environmental mandates like EPA Method 21 and European ISO 15848-1 standards, modern process facilities require valves engineered to minimize fugitive volatile organic compound (VOC) leakage. Our floater ball valve lines feature low-emission packing systems certified to protect atmospheric integrity.
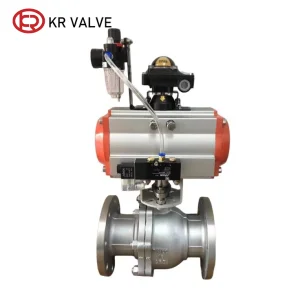
Industrial piping systems increasingly utilize automated flow loops. Our float ball valve design incorporates ISO 5211 direct-mount top flanges, allowing seamless integration with pneumatic single-acting/double-acting actuators, electric motorized gearboxes, and intelligent digital positioners without external bracket adapters.
As an established wholesale OEM factory, our production facilities utilize advanced machining centers and rigorous quality control protocols to guarantee that every valve exiting our assembly line operates flawlessly under design pressure.
The sealing integrity of a floater ball valve hinges on the geometry of the sphere. Utilizing CNC spherical grinding machines, we achieve ball roundness tolerances within 0.01 mm and mirror-finish surface roughness below Ra 0.2 μm, substantially minimizing operating torque while eliminating micro-scratching on polymer seats.
Raw casting integrity is verified via Radiographic Testing (RT), Ultrasonic Testing (UT), Magnetic Particle Inspection (MPI), and Liquid Penetrant Testing (LPT). Positive Material Identification (PMI) using X-ray fluorescence spectrometers confirms alloy composition for high-nickel stainless steels and exotic metals prior to machining.
100% of manufactured valves undergo factory acceptance pressure testing per API 598, ISO 5208, and EN 12266-1 standards. Shell hydrostatic tests are conducted at 1.5x nominal pressure rating, followed by low-pressure air seat tests and high-pressure nitrogen gas tests to guarantee zero bubble leakage.
Our comprehensive valve portfolio is custom-engineered to meet demanding technical parameters across diversely specialized industrial ecosystems.
Engineered with fire-safe API 607/API 6FA features, anti-static grounding springs between ball-stem-body, and NACE MR0175 compliance for sour gas environments containing hydrogen sulfide (H2S).
Full PTFE, PFA, and FEP fluoropolymer lining options isolate corrosive liquid media (hydrochloric acid, caustic soda) completely from metal body components, guaranteeing long service life.
Resilient ductile iron GGG40 bodies and SS316/Duplex trim valves resist high salinity seawater corrosion, delivering optimal flow control in reverse osmosis (RO) desalination plants.
Heavy-duty steel split-body ball valves equipped with metal seats (Stellite / Chrome Carbide coating) effectively manage high-pressure saturated steam and thermal fluid loops.
Global project success demands precise localization. Pipeline installations face dramatically differing geographical, environmental, and regulatory environments—from arctic low-temperature operations to extreme desert conditions.
For sub-zero installations in Nordic regions or high-altitude mining (temperatures down to -46°C), we supply low-temperature carbon steel (ASTM A352 LCB/LCC) bodies fitted with extended bonnet designs that isolate packing seals from freezing fluid zones.
Offshore platform installations undergo multi-layer epoxy coating systems (NORSOK M-501 compliant) to withstand salt-spray exposure. Fasteners and bolting are treated with PTFE/Zinc-Nickel coating to avoid galvanic corrosion.
Our OEM manufacturing lines carry full international certifications, including Pressure Equipment Directive (PED 2014/68/EU), ATEX Directive for explosive atmospheres, SIL 3 Safety Integrity Level qualification, and ISO 9001/14001/45001 management accreditations.
The future of industrial flow control lies in digital connectivity, real-time diagnostic telemetry, and advanced material sciences. Our R&D engineering division is actively pursuing breakthrough valve innovations:
Integrating wireless vibration, temperature, and micro-leak sensors within stem packing housings allows plant operators to monitor valve seat wear dynamically, enabling predictive maintenance before catastrophic line failures occur.
Developing nano-composite matrix seating materials capable of micro-recovering from particulate abrasions, extending soft-seat service lifespans by up to 300% in dirty fluid lines.
Utilizing 3D additive metal printing for complex internal flow-passages and custom trim components in Hastelloy C276 and Titanium, reducing component lead times for emergency plant shutdown replacements.
Detailed answers to essential technical queries raised by piping design engineers, quality assurance managers, and global wholesale purchasers.
Discover our extended line of motorized, actuated, check, pressure relief, and gate valve solutions available for direct wholesale supply.