
Primary Flow Control Equipment for London Projects
Precision-engineered non-return, butterfly, and position-regulated valves certified for municipal water distribution, HVAC networks, and industrial utility corridors across Greater London.
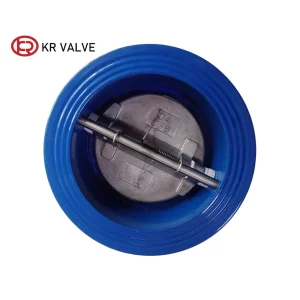
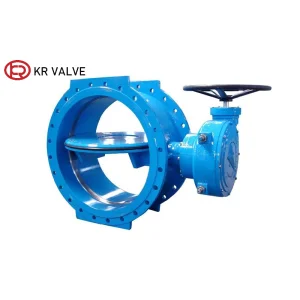
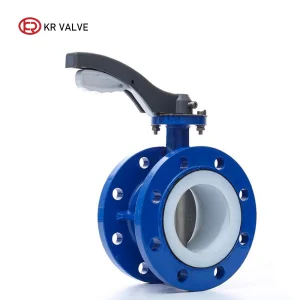
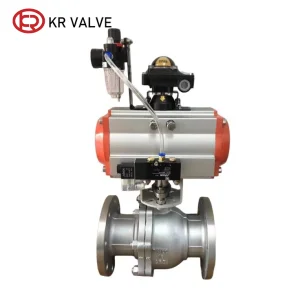
Engineering Valve Resilience for London’s Urban Ecosystem
From Victorian mains modernization to deep-tunnel wastewater management, supply requirements in the UK capital demand exceptional structural integrity and strict regulatory compliance.
Thames Water & AMP8 Rigor
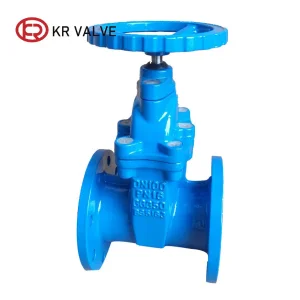
London’s water network operating under Asset Management Period 8 (AMP8) mandates stringent non-revenue water (NRW) reduction. Our BS 5163 resilient seat gate valves feature 100% vulcanized EPDM wedges to ensure permanent zero-leakage isolation under dynamic pressure surges.
Subterranean Space Optimization
Vault space beneath London's financial district (Square Mile) and Westminster is severely constrained. Our Non-Rising Stem (NRS) gate valve configurations drastically reduce vertical headroom requirement without compromising flow area or actuation torque efficiency.
WRAS & UK Environmental Compliance
All non-metallic components contacting potable water adhere strictly to WRAS (Water Regulations Advisory Scheme) standards. Non-toxic fusion-bonded epoxy coatings (FBEC) applied at minimum 250 µm thickness prevent internal tuberculation and bio-film build-up.
Engineering Architecture of BS 5163 Gate Valves
An authoritative comparison of metallurgy, sealing mechanics, and operational standards required for UK civil and industrial procurement.
Selecting the optimal gate valve specification for infrastructure projects within Greater London requires balancing high static head pressure, aggressive soil environments, and maintenance accessibility. As leading direct-to-contractor valve manufacturers, our engineering team adheres strictly to British and European harmonized standards including BS 5163-1 & 2 (Type A and Type B), BS EN 1092-2 flanging, and BS EN 12266-1 pressure testing protocols.
Information Gain Insight for Project Engineers: In urban London retrofit projects where historic grey cast iron mains are converted to modern ductile iron (EN-GJS-500-7), specifying BS 5163 Type B gate valves with high-torque brass stem nuts (CZ132 / CW602N DZR) eliminates galvanically induced stem failure under high chloride subsoil conditions frequently encountered along the Thames estuary.
Technical Comparison Matrix: Resilient Seated vs. Metal Seated Gate Valves
The matrix below outlines the critical operational parameters governing selection across London municipal water mains, central boiler plant rooms, and industrial effluent treatment works:
| Engineering Metric | Resilient Seated Gate Valve (BS 5163) | Metal Seated Gate Valve (DIN 3352 / BS 5163) |
|---|---|---|
| Primary Sealing Mechanism | Ductile Iron wedge fully encapsulated in EPDM / NBR elastomer. | Bronze (LG2 / CC491K) or Stainless Steel (AISI 316) body & wedge trim rings. |
| Flow Resistance & Bore Profile | 100% full-bore straight passage; zero cavity pocket at bottom; minimal Cv head loss. | Recessed bottom body cavity required for wedge seating; susceptible to debris collection. |
| Bubble-Tight Shut-Off Class | BS EN 12266-1 Rate A (Zero allowable leakage rate for gas & liquid). | BS EN 12266-1 Rate C/D (Acceptable micro-leakage rate under high temp). |
| Working Temperature Range | -10°C to +70°C (Potable water, raw water, chilled HVAC). | -10°C to +180°C (High pressure steam, hot thermal oil, heavy industrial process). |
| Internal Coating Protection | Elektrostatik Fusion Bonded Epoxy (FBE) ≥ 250 μm (WRAS approved). | High-temp anti-corrosive primer or bare alloy for petroleum applications. |
| Stem Type & Operations | Non-Rising Stem (NRS) with internal O-ring seal cartridge (replaceable under pressure). | Outside Screw & Yoke (OS&Y) with visual position indication stem. |
Advanced Metallurgy & Coating Engineering for London Environments
Underground pipe networks across London face unique environmental stresses, including ground settlement in clay soils (London Clay Formation) and stray electrical currents from extensive underground railway systems (TfL Tube and Elizabeth Line). To mitigate these challenges, our valve bodies are cast from premium grade Ductile Iron GGG50 (EN-GJS-500-7), offering tensile strengths exceeding 500 MPa and elongation properties above 7%.
For external corrosion protection, every valve undergoes shot blasting to SA 2.5 quality, followed by the thermal application of non-toxic, blue-pigmented epoxy powder coating. This creates an impenetrable dielectric barrier capable of withstanding 3000V spark testing, guaranteeing a operational design life exceeding 50 years under buried UK soil conditions.
Macro Industry Solutions for Tier-1 UK Contractors
Bridging high-capacity direct manufacturing with rapid logistics deployment across the M25 motorway network and Greater London installation zones.
Optimized Total Cost of Ownership (TCO)
By eliminating intermediary markup and sourcing directly from our Tier-1 foundry facilities, EPC buyers and civil engineering firms in London achieve up to 30% reduction in capital expenditure while retaining full EN/BS accreditation and 100% factory inspection testing.
Rapid Delivery & ULEZ Compliance
We work in tandem with UK logistics hubs located in Dartford, Heathrow, and Enfield. Deliveries into London’s Ultra Low Emission Zone (ULEZ) and restricted construction sites (e.g. Silvertown Tunnel, HS2 urban sites) are backed by fully compliant transport management.
Bespoke OEM & Actuator Integration
Every project requires specific operational control. Our valves feature standard ISO 5211 top flanges, enabling seamless direct-mounting of electric (Rotork, AUMA), pneumatic, or hydraulic actuators for remote integration into SCADA control centers.
The Next Decade of Smart Flow Control
Exploring IoT integration, carbon-neutral manufacturing, and digital twin technology for future-ready London infrastructure.
As the UK accelerates its journey toward Net Zero 2050, urban fluid networks are evolving from passive mechanical conduits to highly intelligent, digitally monitored asset matrices. The future of gate valve manufacturing relies on blending robust mechanical design with digital intelligence and ultra-low environmental footprints.
1. Integrated IoT Telemetry & Predictive Leak Detection
Modern smart cities require real-time data visibility. Future iterations of our resilient seated gate valves integrate low-power NB-IoT (Narrowband Internet of Things) sensor arrays within the bonnet housing. These sensors continuously monitor stem position, internal hydrostatic pressure micro-fluctuations, torque resistance signatures, and ambient vibration profiles. By feeding this data into AI-driven predictive maintenance platforms, water utilities can detect acoustic leak anomalies before catastrophic pipe bursts occur in dense metropolitan zones.
2. Eco-Friendly Elastomers & Zero-VOC Coatings
Environmental stewardship requires continuous innovation in raw material synthesis. Traditional vulcanization processes are being upgraded to green EPDM formulations utilizing bio-based ethylene polymers derived from renewable feedstock. Furthermore, zero-VOC (Volatile Organic Compound) powder coatings applied via electrostatic fluid beds reduce manufacturing carbon intensity while delivering enhanced abrasion resistance against abrasive silt carried by raw river water intakes.
3. Additive Manufacturing & Rapid Custom Spares
For urgent repair works across London’s Victorian-era water main infrastructure, standard face-to-face dimensions occasionally fail to align with historical cast iron fittings. Our engineering roadmap includes 3D laser scanning of legacy pipe joints combined with industrial metal 3D printing (Direct Metal Laser Sintering) for custom flange adapters and non-standard gate wedges, cutting emergency turnaround times from months to days.
Extended Flow Control Lineup for UK Engineering
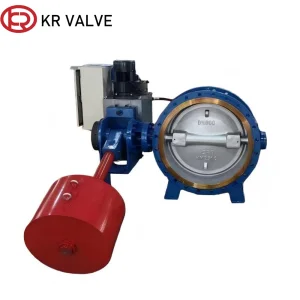
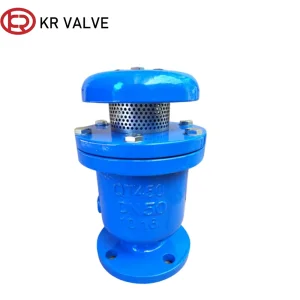
Explore our full range of gate, butterfly, hydraulic control, and exhaust safety valves manufactured to stringent global specifications.
100% Inspected & Certified for UK Peace of Mind
Every gate valve dispatched from our production lines undergoes rigorous quality verification to eliminate project downtime and guarantee site safety.
Hydrostatic Pressure Testing
100% of finished valves are shell tested at 1.5x nominal pressure (e.g. 24 bar for PN16) and seat tested at 1.1x nominal pressure in compliance with BS EN 12266-1 prior to crate packaging.
Full Traceability & 3.1 Certification
Every shipment is accompanied by EN 10204 3.1 Material Test Certificates (MTC), detailing chemical spectrographic analysis and mechanical tensile testing for cast bodies, stems, and wedges.
Direct Engineering Support
Our senior fluid handling engineers provide fast pre-sales technical consultation, CAD dimension drawings, 3D STEP models, and torque calculations tailored for London tender submission packages.
Frequently Asked Questions by London Engineers & Buyers
Get authoritative answers to complex technical queries regarding specification compliance, installation protocols, and international procurement logistics.
What is the key difference between BS 5163 Type A and Type B gate valves for London water projects?
Are your resilient seated gate valves certified for drinking water lines in the UK?
Why choose a Non-Rising Stem (NRS) gate valve over an OS&Y design for subterranean London installations?
What flange drilling standards are compatible with existing UK pipe infrastructure?
How do you guarantee quality control and prevent leakage before shipping to UK sites?
What are the standard lead times for bulk gate valve shipments to Greater London?
Partner with a Trusted Gate Valve Manufacturer for London
Whether you are engineering a major water main expansion, bidding for a Thames Water utility tender, or sourcing high-reliability industrial isolation valves, our engineering team is ready to assist with technical submittals, CAD models, and competitive direct-factory pricing.
Send Inquiry Now