
Featured Industrial Air & Flow Control Valve Series
Explore our top-tier engineered valves optimized for municipal water networks, high-pressure pipelines, industrial exhaust, and heavy-duty flow isolation.
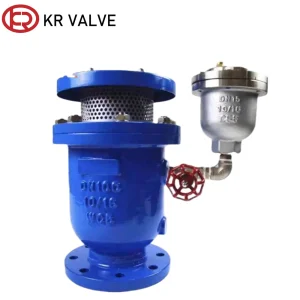
Engineering Dynamics of Custom Air Valve Release Systems
A comprehensive guide on transient flow physics, air entrapment mitigation, and sonic venting design for modern fluid networks.
In municipal water networks, industrial process pipelines, and agricultural irrigation conduits, entrained air represents one of the most destructive yet frequently overlooked operational hazards. Air enters piping systems through pump intakes, sub-atmospheric pressure zones at high elevation peaks, and initial pipe filling sequences. When unmanaged, trapped pocket air shrinks the effective cross-sectional flow area, dramatically increasing head loss, causing severe flow rate instabilities, and triggering high-energy pressure surges—commonly referred to as hydraulic water hammer.
As a premiere Custom Air Valve Release Manufacturer & Factory, our engineering philosophy centers on fluid-structure interaction dynamics. Air release valves are automatically operated mechanical devices designed to perform three vital, distinct functions: releasing pocket air under pressurized operation, exhausting massive volumes of air during line priming, and re-admitting large volumes of atmospheric air during column separation or gravity drainage to prevent catastrophic pipe collapse caused by vacuum formation.
High-Speed Air Exhaust
Specially shaped aerodynamic orifices prevent premature closure (valve slam) when air velocities reach sonic speeds during system startup phase.
Vacuum Relief Protection
Immediate, full-bore air intake capabilities shield thin-walled steel and ductile iron pipes against negative pressure implosions during emergency shutdowns.
Pressurized Micro-Venting
Lever-actuated small orifice mechanisms continually purge tiny accumulated air bubbles even under full working line pressures up to 64 bar.
Custom Air Valve Release Classification Matrix
Selecting the exact air release configuration based on hydraulic mechanics, medium characteristics, and pipe geometry.
| Valve Category | Primary Function | Orifice Size Range | Standard Materials | Target Applications |
|---|---|---|---|---|
| Small Orifice Air Release Valve | Continuous release of dissolved air under line pressure | 1.5 mm – 6.0 mm micro-orifices | Ductile Iron GGG50, SS316 Float, EPDM Seat | High point pipeline ridges, pump discharge headers |
| Large Orifice Air & Vacuum Valve | Bulk venting during filling; massive air intake during drainage | Full Bore (DN25 – DN300) | Cast Steel WCB, Stainless Steel CF8M, NBR/FKM | Raw water transmission, main line drain points |
| Combination Air Release Valve (Triple Function) | Combines small & large orifice capabilities in dual/single chamber | DN50 – DN400 Dual Orifice | Ductile Iron GGG40/50, FBE Coated 300 microns | Long-distance municipal water mains, booster stations |
| Anti-Slam Combination Air Valve | Regulated air venting speed to prevent high-surge liquid impact | DN50 – DN600 Anti-Surge Disc | Super Duplex SS, Alloy Steel, Reinforced Polycarbonate | High-head pumping lines, surge protection zones |
| Sewage & Wastewater Air Valve | Vents air while keeping solid debris away from sealing mechanisms | Elongated Body (DN50 – DN200) | 316L SS Body, Conical Lower Body, Bronze Trim | Slurry handling, wastewater lift stations, effluent lines |
China Factory & Supply Chain Infrastructure Advantages
How our Tianjin manufacturing ecosystem delivers unmatched technical precision, raw material integrity, and cost efficiencies.
As a leading Chinese valve manufacturing hub, Tianjin provides a fully integrated industrial ecosystem encompassing world-class metallurgic foundries, automated precision CNC machining centers, and advanced chemical coating facilities. Our custom air valve release factory leverages this robust supply chain cluster to achieve unrivaled quality control and cost competitiveness.
Unlike standard assembly shops, our enterprise manages the total production value chain: from spectrographic metallurgy verification of molten Ductile Iron (GGG40/GGG50) and WCB Cast Steel, to precision investment casting of Stainless Steel (CF8/CF8M/CF3M) floats and anti-slam internals. Every valve housing undergoes 100% hydrostatic shell testing at 1.5 times nominal pressure and seat leak testing according to ISO 5208 and EN 12266-1 standards.
Metallurgical Precision
Optical emission spectrometry ensures exact chemical composition, tensile strength, and elongation properties for all ductile iron and alloy castings.
Electrostatic Epoxy Coating
Automated fluidized bed Fusion Bonded Epoxy (FBE) coating guarantees a minimum 250–300 micron non-toxic barrier complying with potable water safety standards.
5-Axis CNC Machining
Micron-level dimensional tolerances on valve seats, float guides, and stem threads eliminate air friction leakage and mechanical binding.
Localization Support, Certification & Compliance Guarantee
Empowering international engineering contractors and local water authorities with globally accredited custom valve builds.
Deploying flow control equipment across international boundaries requires strict compliance with regional hydraulic, sanitary, and structural regulations. As a dedicated OEM/ODM manufacturer, we offer full custom engineering adaptation to meet local municipal requirements across North America, Europe, the Middle East, South America, and Southeast Asia.
Potable Water Hygiene
Our elastomer seals (EPDM, NBR, Silicone) and epoxy coatings are certified under WRAS (UK), NSF/ANSI 61 (USA), and DVGW (Germany) for safe drinking water applications.
- Zero toxic leaching
- Microbiological growth resistant
- Cleanroom assembly option
International Design Standards
Valves are fully engineered to comply with AWWA C512, EN 1074-4, BS EN 12627, DIN 3202, and ANSI/ASME B16.42 flange connection standards.
- Flange Drilling: PN10, PN16, PN25, PN40, ANSI 150/300
- Threaded Ports: NPT, BSPT, BSPP
- Custom face-to-face dimensions
Comprehensive Documentation
We provide complete engineering dossiers required by EPC contractors for government tenders and project sign-offs.
- EN 10204 3.1 Material Test Reports
- Hydrostatic & Air Venting Test Curves
- 3D CAD / BIM Step Models
Global Procurement & Total Cost of Ownership (TCO) Optimization
Direct factory sourcing models designed to minimize capex while ensuring 30+ year maintenance-free valve service life.
For global engineering procurement contractors (EPCs) and municipal asset managers, initial valve procurement cost represents only a fraction of total lifecycle expenditure. Unreliable air release valves lead to premature pipe bursting, continuous energy consumption due to air-lock friction head loss, and expensive emergency downtime.
By partnering directly with our custom air valve release manufacturing facility in China, institutional buyers eliminate multi-tier distributor markups while securing custom-engineered features tailored to unique fluid pressure profiles.
| Procurement Pillar | Traditional Trading Channel | Direct Factory Strategic Partnership |
|---|---|---|
| Design Customization | Off-the-shelf catalog limitations only | 100% Custom orifice sizing, non-standard materials, custom painting & branding |
| Quality Traceability | Third-party batch sampling | Direct 100% individual pressure testing with video/digital MTR records |
| Supply Chain Lead Time | 12 – 20 Weeks via global agents | 4 – 6 Weeks optimized direct factory production schedules |
| Project Lifecycle TCO | High risk of air leak & frequent maintenance | Optimized self-cleaning float mechanics with 30-year operational life |
Industry Innovation: Smart IoT Air Release & Anti-Slam Technology
Integrating digital diagnostic sensors and dynamic fluid-dampening mechanisms for next-generation smart water grids.
Smart IoT Sensor Integration
Optional integration of wireless pressure transducers, acoustic leak detection sensors, and float position indicators connected to municipal SCADA systems for real-time health monitoring.
Anti-Slam Surge Attenuation
Advanced dual-stage discharge mechanism allows rapid air exit until liquid approaches, switching instantly to a restricted micro-orifice to cushion water column impact and eliminate pressure spikes.
Eco-Polymers & Anti-Corrosion
Next-generation lightweight composite floats made from solid cellular polypropylene eliminate puncture risks associated with hollow metal floats in highly aggressive chemical environments.
Localized Industrial Application Scenarios
Tailor-made air management valve designs implemented across diverse environmental and engineering operating conditions.
1. Municipal Water Supply Lines
Installed at geographic peaks, long flat runs, and pump discharge outlets to prevent air locks, maintaining maximum pump pumping capacity and reducing electrical power draw.
2. Wastewater & Sewage Networks
Custom elongated body air valves ensure sewage liquids and solid scum remain below the upper sealing assembly, eliminating clogging and environmental methane leaks.
3. Desalination & Marine Piping
High-grade Super Duplex SS2507 and Titanium trimmed air valves withstand harsh seawater corrosion and high-salinity cavitation environments.
4. High-Rise HVAC Chilled Water
Compact automatic air vents clear micro-bubbles from closed loop heating and cooling circuits, preventing radiator noise, pump impeller erosion, and heat exchanger inefficiency.
5. Agricultural Irrigation Schemes
Cost-effective, high-flow air vacuum valves protect drip irrigation tubing and main PVC pipelines from vacuum collapse during rapid system drain-down cycles.
Complementary Industrial Valves & Control Solutions
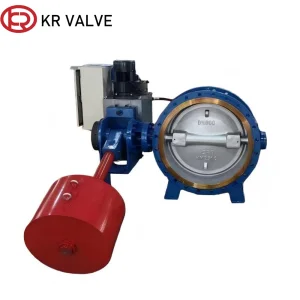
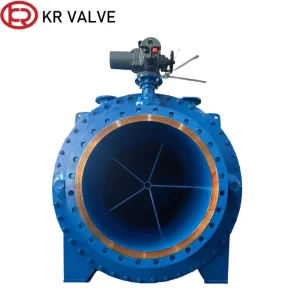
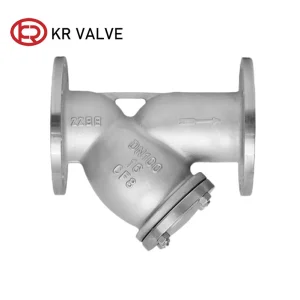
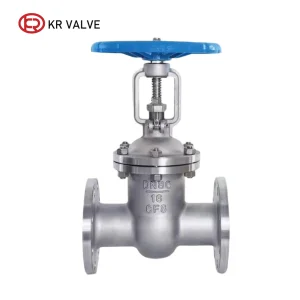
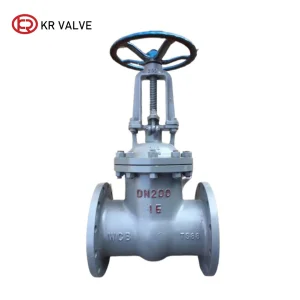
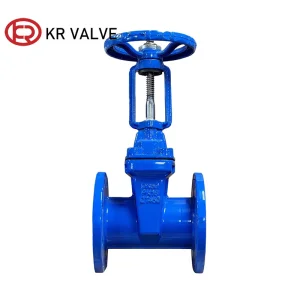
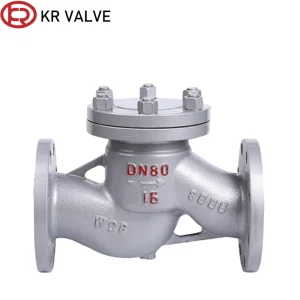
Select from our extensive inventory of hydraulic control valves, gate valves, check valves, and strainers built for global pipeline projects.
Frequently Asked Questions (FAQ)
Expert answers to technical procurement, sizing, installation, and manufacturing questions regarding custom air valve release systems.