
Industrial Grade SS Gate & Steel Flow Control Valves
Explore our top-tier engineered valves designed for rigorous pressure classes, harsh chemical environments, and critical municipal pipelines.
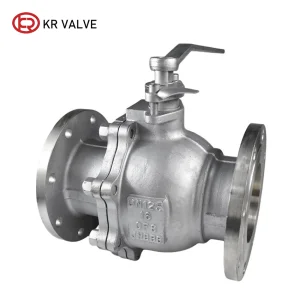
OEM China SS304 Floating Ball Valve Manufacturers - Flange Type Suppliers from Factory, DN50-DN300, PN16/PN25 Manufacturer, Factories
View Specs & Quote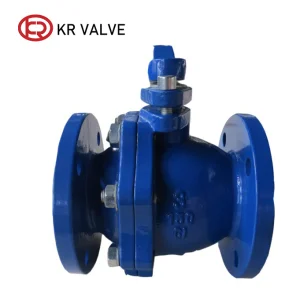
Custom Ductile Iron Flange Ball Valve with PTFE Seat - China Suppliers & Factory, PN16/PN25, Sizes DN50-DN300 Supplier, Manufacturer
View Specs & Quote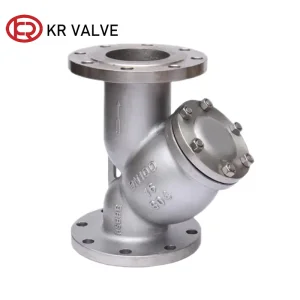
Wholesale Y type strainer SS304 material 150LB flanged basket filter Suppliers, Factories
View Specs & Quote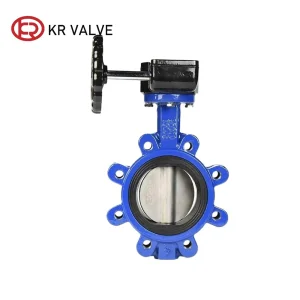
Custom Gear Box Operation Lug Butterfly Valve EPDM Seal Supplier, Factory
View Specs & Quote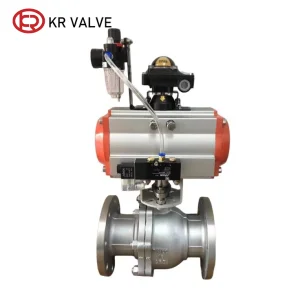
Custom China Pneumatic Ball Valve with Positioner & Limit Switch - Quality Suppliers & Factory Direct Options Manufacturer, Factory
View Specs & Quote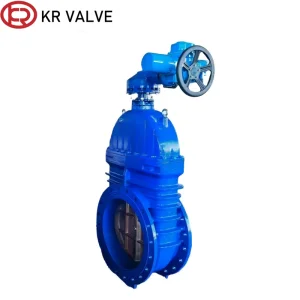
OEM Electric operation brass metal seat GGG40 gate valve Suppliers, Factory
View Specs & Quote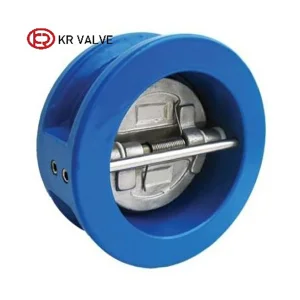
Wholesale China Suppliers Factory One Way Valve, Ductile/Cast Iron Body CF8 Disc, Wafer Type, DN40-DN700, PN6/PN25 Suppliers, Manufacturers
View Specs & Quote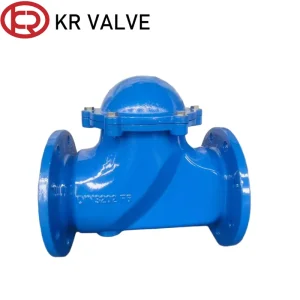
OEM Ball type one way valve with soft seal ball PN16 Factories, Factory
View Specs & QuoteMacro-Industrial Overview: Stainless Steel & Cast Steel Gate Valves
In modern industrial process engineering, fluid control infrastructure dictates plant safety, longevity, and operational efficiency. OEM Stainless Steel (SS) and Cast Steel Gate Valves represent the critical backbone of isolation systems worldwide.
Energy & Petrochemical Refining
High-pressure cast carbon steel (WCB, WC6) and stainless steel (CF8M/SS316) gate valves are mandatory for crude oil transmission, cracking towers, and steam lines where zero fugitive emissions and zero pressure loss under full flow are essential.
Desalination & Municipal Water Infrastructure
Chloride-rich seawater desalination requires Duplex SS (2205/2507) and SS316 gate valves. Resilient seat gate valves engineered with EPDM encapsulation prevent bio-fouling and internal corrosion across urban distribution grids.
Hygienic Food, Beverage & Pharma
Electropolished SS304/SS316L gate valves and sanitary ball/strainer assemblies comply with strict FDA and EHEDG standards, guaranteeing smooth internal bores that prevent bacterial accumulation and facilitate CIP (Clean-in-Place) protocols.
OEM Competitive Advantage: By integrating advanced investment casting (lost-wax technique) for stainless steel and automated sand-casting lines for heavy-duty cast steel bodies, leading Chinese OEM valve factories offer optimal wall thickness tolerances, zero porosity, and superior fatigue resistance under thermal cycling.
Metallurgical Benchmarks & Engineering Specifications
Selecting the correct steel composition, stem design, and wedge architecture determines whether a gate valve achieves a 20-year service life or suffers premature seat degradation.
| Material / Component | Equivalent Grade (ASTM / EN) | Tensile Strength (MPa) | Recommended Medium | Temperature Range |
|---|---|---|---|---|
| SS304 Stainless Steel | ASTM A351 CF8 / EN 1.4308 | ≥ 485 MPa | Potable Water, Weak Acids, Organic Solvents | -196°C to +425°C |
| SS316 Stainless Steel | ASTM A351 CF8M / EN 1.4408 | ≥ 485 MPa | Seawater, Chlorides, Nitric & Acetic Acids | -196°C to +538°C |
| Duplex Stainless Steel | ASTM A890 4A / EN 1.4462 (2205) | ≥ 655 MPa | Brine, Mining Slurry, Concentrated H2SO4 | -40°C to +300°C |
| WCB Cast Carbon Steel | ASTM A216 WCB / 1.0619 | ≥ 485 MPa | Non-corrosive Oil, Gas, High-Pressure Steam | -29°C to +425°C |
| Ductile Iron (GGG40) | QT450-10 / EN-GJS-400-15 | ≥ 400 MPa | HVAC Water, Sewage, Fire Protection Lines | -10°C to +120°C |
Rising Stem vs. Non-Rising Stem (NRS) Design Mechanics
Rising Stem (OS&Y - Outside Screw and Yoke): The stem turns and moves up/down outside the valve body, providing immediate visual verification of open/close positions. Threaded stem portions reside away from fluid flow, reducing thread erosion and corrosion caused by aggressive media. Mandatory in refinery and high-pressure chemical installations.
Non-Rising Stem (NRS): The stem turns inside the valve body, causing the wedge to travel upward along the internal stem threads. Ideal for space-constrained environments such as underground municipal water mains, shipboard piping, and subterranean valve vaults.
Wedge Sealing Dynamics: Flexible vs. Solid vs. Resilient
Flexible Wedge: Cast with a narrow cut around the perimeter to allow slight elastic deformation. This compensates for pipe stress, thermal expansion, and seat misalignment, preventing valve binding in high-temperature steam systems.
Resilient Seat (EPDM / NBR Encapsulated): The ductile iron or steel disc is fully bonded with vulcanized EPDM or NBR rubber. Provides zero-leakage (Bubble-Tight Shutoff Class VI) and smooth bottom passage without debris-trapping recesses.
Strict QC Controls, NDT Inspection & Standards Compliance
As a direct OEM factory partner, we maintain rigorous quality oversight at every stage of production—from spectrographic raw material validation to final hydrostatic testing.
100% Hydro Testing
Every gate, ball, check, and butterfly valve undergoes shell testing at 1.5x PN rating and seat leakage testing at 1.1x PN rating according to API 598 and EN 12266-1 standards.
PMI & NDT Inspections
Positive Material Identification (PMI) guarantees exact nickel/chromium ratios in SS304/SS316 alloys. Ultrasonic (UT) and Radiographic (RT) testing rule out casting voids.
International Certifications
Fully compliant with API 600, API 6D, DIN 3352 F4/F5, BS 5163, ISO 5211 actuator mounting flanges, ASME B16.34 pressure rating, and CE PED accreditation.
Localized Global Logistics
Export-grade fumigated wooden case packaging, customs clearance assistance, FOB/CIF/DDP incoterms flexibility, and full material test report (MTR) traceability.
The Future of Intelligent Flow Control & Surface Engineering
As industrial processes shift toward automation, decarbonization, and smart infrastructure, valve manufacturing is undergoing a significant transformation.
Smart Sensor Integration
IoT-enabled position switches, acoustic leak detectors, and real-time stem torque monitors embedded directly into motorized gate valve bonnets allow predictive maintenance.
Low Fugitive Emissions
Strict environmental regulations demand API 622 / API 641 fugitive emission testing. Modern packing rings utilize die-formed flexible graphite with anti-extrusion braided end rings.
Stellite HVOF Hard-Facing
High-Velocity Oxygen Fuel (HVOF) thermal spraying of Cobalt-base Stellite alloy on stainless steel seats dramatically increases wear resistance against abrasive slurries.
Fusion Bonded Epoxy (FBE)
Electrostatic application of non-toxic, WRAS/NSF61 approved epoxy coatings (minimum 250μm dry film thickness) protects cast steel and ductile iron against chemical soil corrosion.
Specialized Heavy-Duty & Actuated Valves
Complete pipeline systems require custom actuators, large diameter gate valves, non-return check valves, and hydraulic control solutions.
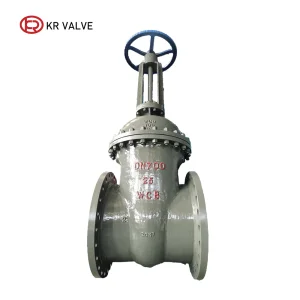
Custom DN700 WCB Cast Steel Flange Gate Valve Supplier, Factory
View Specs & Quote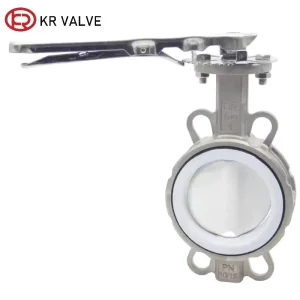
OEM Wafer butterfly valve PTFE lined seat and SS body Supplier, Suppliers
View Specs & Quote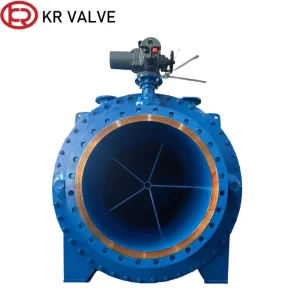
OEM Electric cone valve used for big size water control Suppliers, Manufacturer
View Specs & Quote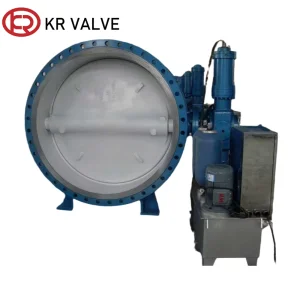
Custom Heavy hammer hydraulic butterfly valve triple eccentric type Manufacturers, Factory
View Specs & Quote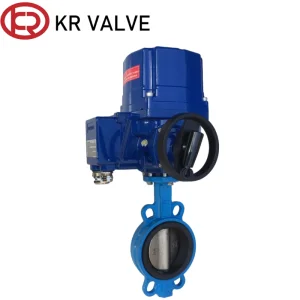
Wholesale Electric Actuated Butterfly Valve Wafer EPDM Seal Type Motorized Suppliers, Factory
View Specs & Quote
OEM Pneumatic Ball Valve With Positioner and Limit Switch Suppliers, Factory
View Specs & Quote
Custom China DN700 WCB Cast Steel Flange Gate Valve Suppliers - High Torque with Flexible Actuation from Factory Supplier, Factories
View Specs & Quote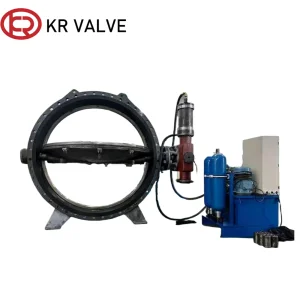
Custom Adjustable Hydraulic Butterfly Valve by China Suppliers - Double Eccentric Type from Factory, DN200-DN3000 Suppliers, Manufacturers
View Specs & QuoteFrequently Asked Questions (FAQ)
Expert answers regarding engineering selection, material selection, standard compliance, and custom OEM manufacturing.