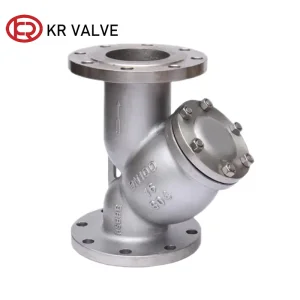
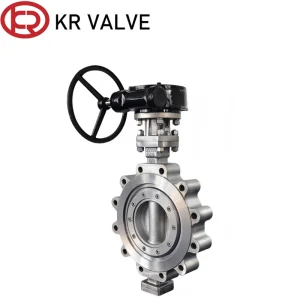
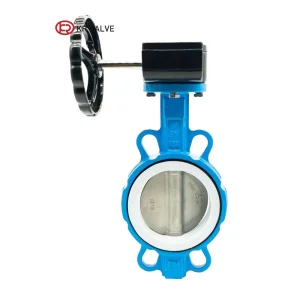
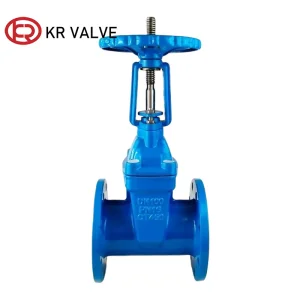
Industrial Valve Catalogue (Part I)
Explore our core manufactured valves certified to DIN, BS, ANSI, and AWWA specifications for high-reliability applications.
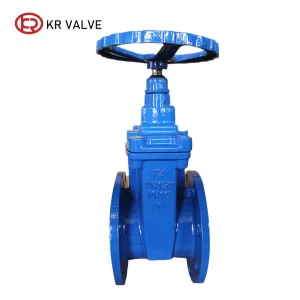
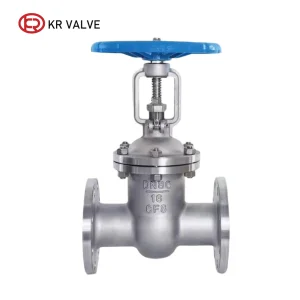
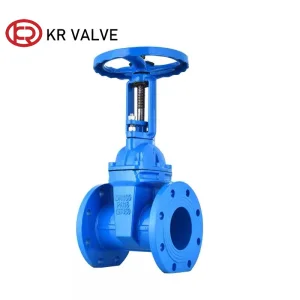
Technical Architecture & Mechanics of Non-Rising Stem (NRS) Gate Valves
An in-depth mechanical breakdown of NRS gate valve engineering, stem sealing mechanisms, and material metallurgy for high-pressure fluid networks.
Internal Stem Thread Engineering
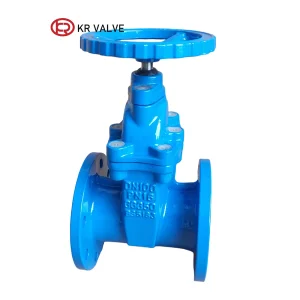
Unlike Rising Stem (RS) valves where the stem lifts out of the bonnet during operation, Non-Rising Stem (NRS) gate valves utilize an internal thread mechanism. The stem rotates within the valve body, causing the wedge nut to travel vertically along the threaded stem inside the fluid chamber.
Vulcanized EPDM Resilient Seating
Modern NRS gate valves feature a fully encapsulated ductile iron wedge (EN-GJS-500-7) coated with high-grade EPDM elastomer via advanced hot vulcanization processes. This design ensures zero seat pocket accumulation and guarantees bi-directional bubble-tight shut-off (Class A leakage integrity according to ISO 5208).
Multi-O-Ring Stem Sealing Technology
To eliminate stem leakage—a common vulnerability in traditional packed gland valves—our wholesale NRS gate valves incorporate a triple O-ring sealing gland made of NBR/EPDM combined with a brass thrust collar. This allows stem seal maintenance under full operational line pressure without shutting down the main network.
Technical Specification Matrix: Resilient Seated NRS Gate Valves
| Parameter / Standard | DIN 3352 F4 / F5 | BS5163 Type A/B | AWWA C515 / C509 | EN 1074-1 & 2 |
|---|---|---|---|---|
| Nominal Size Range | DN50 - DN1200 (2" - 48") | DN50 - DN600 (2" - 24") | NPS 2" - NPS 36" | DN40 - DN1000 |
| Nominal Pressure (PN) | PN10 / PN16 / PN25 | PN10 / PN16 / PN25 | Class 150 / 250 PSI / 300 PSI | PN10 / PN16 / PN25 |
| Body Material Options | Ductile Iron GGG50 / GGG40 | Ductile Iron EN-GJS-500-7 | Ductile Iron ASTM A536 | EN-JS1050 / Cast Steel WCB |
| Stem Metallurgical Spec | Stainless Steel 420 / 304 / 316 | Stainless Steel 410 / 316 | Dezincification Resistant Brass / SS316 | AISI 420 / Duplex SS |
| Coating Specification | Fusion Bonded Epoxy (FBE) ≥ 250μm | FBE Coating RAL 5005 / RAL 5017 | AWWA C550 Compliant FBE | WRAS / DVGW Certified Epoxy |
| Testing Pressure (Shell / Seat) | 1.5 x PN / 1.1 x PN (Hydrostatic) | 1.5 x PN / 1.1 x PN | 2.0 x CWP / 1.0 x CWP | ISO 5208 Rate A (0 Leakage) |
Macro Industry Solutions & Field Applications
Discover how wholesale NRS gate valves form the backbone of modern municipal, industrial, and specialized infrastructure networks globally.
Municipal Potable Water Distribution
Municipal drinking water distribution networks require isolation valves that resist internal corrosion and bio-film build-up. Our non-rising stem gate valves utilize non-toxic, WRAS-approved fusion-bonded epoxy linings and lead-free stem nuts, preventing contamination while supplying zero-leakage reliability under continuous city line pressure.
Underground Burial & Vault Installations
Because the stem length remains constant regardless of whether the valve is open or closed, NRS gate valves can be fitted with extension spindles and buried directly underground or installed inside compact concrete street vaults. Operators can control the valve from ground level using T-key extension rods.
Fire Protection & UL/FM Standpipe Systems
Underground fire main loops demand instantaneous response and uninterrupted flow rate capabilities during emergency situations. Our AWWA standard NRS gate valves, configured with indicator posts (PIV ready), offer robust emergency isolation for industrial facilities, refineries, and high-rise commercial complexes.
China Factory 4.0: Supply Chain Resilience & Production Scale
Combining automated precision casting, CNC multi-axis machining, and rigorous quality verification to supply wholesale volume with zero defect rate.
Automated Resin Sand Casting & Metallurgy Control
Our Tianjin production hub employs state-of-the-art resin sand molding lines paired with spectrographic chemical analysis for every iron heat. By precisely controlling the nodularity of Ductile Iron (EN-GJS-500-7 grade ≥ 90% nodularity), we ensure our valve bodies withstand pressure surges, thermal expansion stress, and external earth loadings without micro-cracking.
Full-Chain Supply Control & Rapid Lead Times
By managing raw material inventory, machining, epoxy coating, assembly, and hydrostatic testing in-house, we eliminate sub-supplier bottlenecks. Global EPC contractors and valve distributors benefit from predictable delivery schedules, containerized volume packing, and comprehensive OEM/ODM private labeling services.
NRS Gate Valve Technology Roadmap & Future Outlook
Pioneering smart digital sensing, advanced elastomer formulations, and eco-friendly manufacturing technologies for the next generation of flow control.
IoT-Enabled Smart Position Monitoring
Integration of low-power magnetic stem encoders inside the bonnet cavity allows wireless transmission of exact valve open/close percentages to SCADA systems, eliminating blind operations in buried municipal networks.
Self-Healing Nano Elastomers
Developing next-generation EPDM compound matrices engineered with fluoropolymer additives. These self-healing resilient wedges offer superior abrasion resistance against grit, sand, and particulate-laden untreated water.
Carbon-Neutral Casting Processes
Transitioning furnace power to green electric induction melting and implementing closed-loop sand reclamation systems to reduce scope 1 and scope 2 manufacturing emissions by 40% by 2030.
Global Regulatory Compliance & Total Cost of Ownership (TCO)
How direct factory-wholesale sourcing lowers life-cycle expenditure while ensuring compliance with international engineering codes.
Regulatory Certification & International Approval
Cross-border procurement requires strict adherence to localized engineering and health certifications. Our NRS gate valves are designed to pass rigorous THIRD-PARTY audits including ISO 9001:2015, CE PED 2014/68/EU certification, WRAS (UK) drinking water testing, and compliance with API 598 pressure inspection standard.
- Standard Flange Drilling: EN1092-2 (PN10/PN16/PN25), ANSI B16.1 Class 125/150, BS4504
- Face-to-Face Dimensions: EN 558-1 Series 14 (DIN 3352 F4), Series 15 (DIN 3352 F5), ASME B16.10
- Hydrostatic Shell & Seat Certification furnished with every mill inspection certificate (EN 10204 3.1)
Total Cost of Ownership (TCO) Analysis
While initial acquisition price is vital, life-cycle costs are dominated by maintenance labor, downtime losses, and energy consumption caused by valve friction:
Frequently Asked Questions (Technical Q&A)
Comprehensive engineering insights into NRS gate valve selection, installation, and operation.
What is the key functional difference between Non-Rising Stem (NRS) and Rising Stem (RS) gate valves?
The fundamental distinction lies in stem movement and thread position. In a Non-Rising Stem (NRS) valve, the stem threads are located inside the body media chamber; when turned, the stem rotates in place while the gate moves up or down along the stem threads. In a Rising Stem (RS) valve, the stem threads are external (Outside Screw and Yoke - OS&Y), and the entire stem rises linearly out of the bonnet as the valve opens. NRS valves are preferred when space overhead is restricted or when installed underground with extension spindles.
How does an EPDM resilient seated NRS gate valve prevent debris accumulation compared to metal seated valves?
Traditional metal-seated gate valves rely on a bottom body recess/groove to catch the metallic wedge. Over time, sediment, sand, and scale accumulate in this groove, preventing tight valve closure. Resilient seated NRS gate valves feature a flat, smooth body bottom bore; the rubber-encapsulated ductile iron wedge compresses directly against the smooth body cavity, allowing pipeline solids to be flushed straight through without trapping debris.
Can NRS gate valves be customized with different flange standards and actuation methods?
Yes. As a direct wholesale manufacturer, we provide OEM customization for flange dimensions including EN 1092-2 (PN10/PN16/PN25), ANSI B16.1 / B16.42 Class 125/150, BS10 Table E, and JIS 10K/16K. Furthermore, while standard operation is by handwheel or T-key cap, our NRS valves can be fitted with ISO 5210 top mounting flanges for electric multi-turn actuators (e.g., AUMA, Rotork) or bevel gearboxes.
What quality inspection procedures are performed before shipment?
Every valve manufactured in our factory undergoes 100% hydrostatic and pneumatic testing according to ISO 5208 and API 598. Shell tests are conducted at 1.5 times the nominal working pressure (e.g., 24 Bar for PN16 rating), and seat tightness is tested at 1.1 times the nominal working pressure with zero allowable leakage. Spark testing is also conducted on the 250μm fusion-bonded epoxy coating to verify dielectric seal thickness.
Industrial Valve Catalogue (Part II)
Browse our specialized check, strainers, control, and butterfly valve series ready for factory-direct bulk procurement.