
Featured Custom Ball Valve & Flow Control Solutions
Factory-direct OEM & ODM pipeline valves built to DIN, ANSI, AWWA, and BS international engineering standards.
Macro-Industry Flow Control Solutions & Infrastructure Dynamics
Analyzing global municipal water networks, high-pressure industrial pumping systems, and advanced fluid containment technologies.
In modern hydraulic infrastructure, custom ball valves for water systems serve as critical active nodes that determine overall grid efficiency, operational safety, and life-cycle capital expenditure. As global water management shifts toward smart distribution networks and continuous high-pressure conveyance, fluid control equipment must withstand severe dynamic stress, violent pressure surges (water hammer), corrosive media, and demanding cycle frequencies without structural fatigue or seat degradation.
Standard off-the-shelf valves often fail to meet specialized hydraulic profiles. Variations in water chemistry—such as high chloride concentrations in brackish intake lines, elevated scaling potential in hard municipal water, or chemical dosing in industrial wastewater—require tailored metallurgical selections, engineered flow path geometries, and specialized seat polymers. Factory-customized ball valves eliminate fluid turbulence and localized pressure drops by maintaining a continuous, unobstructed full-bore flow profile, drastically reducing energy consumption across high-capacity pumping stations.
Hydraulic Cavitation Suppression
Custom multi-stage trim geometry dissipates fluid kinetic energy progressively, preventing damaging cavitation bubbles from collapsing against metallic valve body walls during differential pressure throttling.
Zero-Headloss Full Port Architecture
Precision CNC-machined solid balls match the exact internal pipe diameter, achieving a friction factor ($K$-value) approaching zero to optimize pump efficiency in long-distance water transmission lines.
Bi-Directional Bubble-Tight Sealing
Dual-seat spring-energized or pressure-assisted sealing mechanisms maintain zero leakage across upstream and downstream pressure differentials, complying with ISO 5208 Rate A and API 598 standards.
Metallurgical Science & Seat Polymer Customization
Comprehensive material matrix tailored for raw water, potable water, brackish intake, and aggressive industrial effluents.
Selecting appropriate body alloys, stem packings, and seat inserts is critical to preventing premature valve failure caused by galvanic corrosion, erosion-corrosion, or chemical degradation. As a specialized custom ball valve manufacturer, our engineering team utilizes high-purity casting techniques, vacuum heat treatment, and precision polymer molding to ensure maximum service life.
| Component | Material Options | Technical Characteristics | Recommended Water Application |
|---|---|---|---|
| Valve Body | Ductile Iron GGG40 / GGG50 Cast Steel WCB (A216) SS304 / SS316 (CF8/CF8M) Duplex 2205 / 2507 |
High tensile strength, fusion-bonded epoxy coating (EP-F) >250μm, superior pressure containment, shock resistance. | Municipal Mains Desalination High-Rise HVAC |
| Internal Ball | SS304 / SS316 Stainless Steel Electroless Nickel Plated (ENP) Super Duplex Stainless Steel Stellite / Chrome Carbide Coated |
Mirror-polished surface finish ($Ra < 0.2\mu m$), high roundness tolerance (<0.01mm), exceptional erosion barrier. | Brackish Water High-Velocity Pumps Slurry Lines |
| Seat Rings | Virgin PTFE / Reinforced R-PTFE PEEK (Polyetheretherketone) NBR / EPDM Resilient Seals Metal-to-Metal Hard-Faced |
Low friction coefficient, anti-extrusion geometry, thermal stability up to 260°C, zero-bubble seal performance. | Potable Drinking Water Thermal Fluid Chemical Dosing |
| Stem Assembly | 17-4PH Stainless Steel SS316 / Duplex 2205 Monel K500 Alloy |
Blowout-proof stem design, live-loaded V-ring PTFE packing, integrated anti-static grounding spring device. | High-Cycle Automation Underground Vaults |
Global Compliance Assurance & Localization Support
Ensuring full regulatory compliance across regional water authorities, international trade bodies, and environmental directives.
Potable Water Hygiene
Certified lead-free construction complying with NSF/ANSI 61 and NSF/ANSI 372 standards for drinking water distribution in North America, alongside WRAS (UK), DVGW W270 (Germany), and ACS (France) compliance.
Pressure & Flange Standardization
Custom flange end connections machined precisely to EN 1092-1 (PN10/16/25/40), ASME B16.5 (Class 150/300/600), AWWA C507, and JIS B2220 to allow seamless integration into existing regional piping layouts.
100% Quality Hydro-Testing
Every custom valve undergoes factory shell hydrostatic testing at 1.5x working pressure and seat tightness testing at 1.1x working pressure per EN 12266-1 and API 598 prior to export packaging.
Targeted Application Scenarios in Water Management
Field-proven performance across municipal, commercial, agricultural, and heavy industrial water processing sectors.
1. Municipal Water Treatment & High-Pressure Distribution Networks
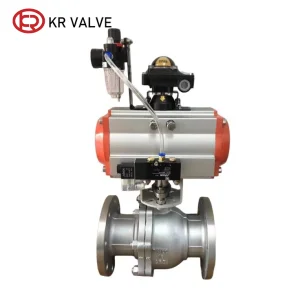
In large-scale city water utility grids, custom ball valves are deployed at main pumping stations, pressure-reducing vaults, and reservoir isolation mains. Their full-bore flow profile minimizes pumping energy consumption while resilient EPDM/PTFE seats guarantee bubble-tight isolation during system repairs. Integrated electric and pneumatic positioners allow central SCADA systems to regulate line pressures dynamically.
2. Seawater Reverse Osmosis (SWRO) Desalination Plants
Desalination processes involve aggressive high-chloride seawater operating under extreme pressures (up to 80 bar). Custom ball valves manufactured from Super Duplex Stainless Steel (UNS S32750 / 2507) or Nickel-Aluminum Bronze provide complete immunity to pitting and crevice corrosion, maintaining zero seat degradation despite high fluid velocities.
3. District Cooling, HVAC & Industrial Process Water Loops
Commercial high-rise hydronic loops and industrial cooling towers require rapid-acting automated valves to balance thermal loads. Custom motorized ball valves featuring ISO 5211 direct-mount actuator flanges, anti-static grounding, and high-temperature R-PTFE seats enable precise modulations over hundreds of thousands of operational cycles without stem packing leaks.
Technology Roadmap & Future Outlook (2025–2030)
Pioneering smart digital valve diagnostics, eco-friendly metallurgy, and zero-emission fluid containment.
IoT-Integrated Smart Valve Sensing
Incorporating wireless piezoelectric vibration sensors, stem torque transducers, and seat acoustic leak detectors directly into the valve body to provide predictive maintenance telemetry to cloud analytics platforms.
Zero-Fugitive Emission Stem Packing
Advancing live-loaded Belleville spring packing sets designed to comply with ISO 15848-1 Class AH standards, eliminating VOC and micro-leakage risks in sensitive chemical water treatment plants.
Nanocomposite Self-Healing Seats
Developing next-generation polymer seat blends infused with micro-encapsulated fluoropolymers that automatically seal microscopic surface scratches caused by abrasive sand particles in raw river water.
Frequently Asked Questions (Engineering Q&A)
Expert insights regarding specification selection, OEM customization, and maintenance of custom water ball valves.
Explore Additional Industrial Pipeline Equipment
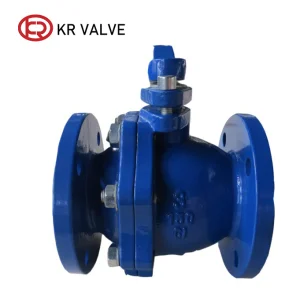
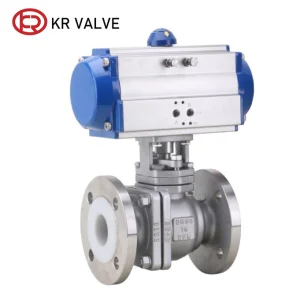
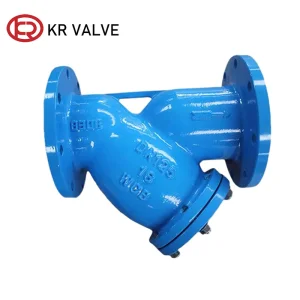
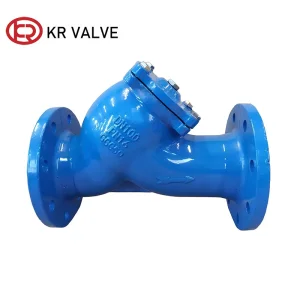
High-performance check valves, strainers, butterfly valves, and control valves from our integrated factory lines.
Request Custom Ball Valve Technical Drawings & Factory RFQ
Consult directly with our fluid control application engineers to specify pressure class, seat polymers, flange dimensions, and smart actuation accessories for your water project.
Contact Engineering Team