Standard-Compliant Resilient Seat Gate Valves for Austria
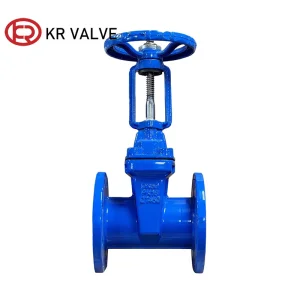
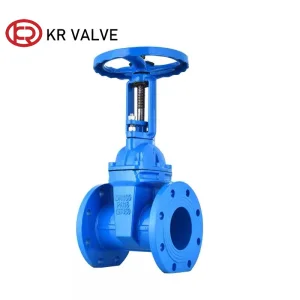
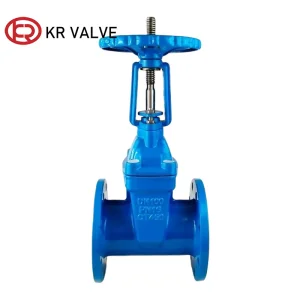
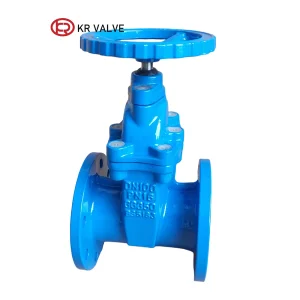
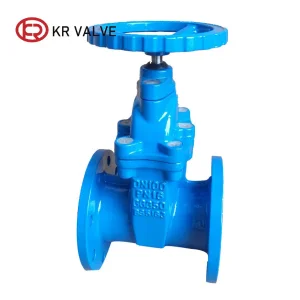
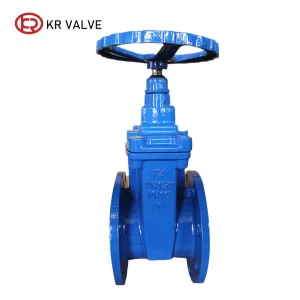
Direct factory-manufactured DIN F4, DIN F5, and BS5163 soft-sealed gate valves featuring vulcanized EPDM wedges, zero-cavity flow paths, and GSK-certified epoxy coatings.
Austria’s Water & Industrial Infrastructure Demands High-Integrity Flow Control
Austria’s commitment to ultra-pure municipal water supply (ÖVGW compliance), high-head alpine hydroelectric infrastructure, and stringent environmental regulations requires specialized valve engineering that withstands extreme working pressures and freezing mountain climates.
Alpine Municipal Water & Utility Directives
Austrian municipal water networks—operated by major entities like Wiener Wasser, LINZ AG, Holding Graz, and Salzburg AG—rely heavily on mountain spring water distributed under substantial static hydraulic heads. Resilient seat gate valves installed in these networks must operate with absolute zero seat-leakage under pressure ratings up to PN16 and PN25.
Furthermore, underground pipeline networks across Tyrol, Vorarlberg, and Carinthia experience severe frost penetration during alpine winters. Valves must feature deep-burial capabilities, maintenance-free O-ring stem seals, and full-bore passage to prevent sediment accumulation during seasonal thaw cycles.
- ÖVGW & EN 1074 Compliance: Meets strict European drinking water standards and ÖVGW W 1.35 hygiene parameters.
- Sub-Zero Temperature Resistance: Ductile iron EN-GJS-400-15 body castings engineered for alpine ground freeze conditions down to -20°C.
- Hydropower & Snowmaking Utility: Handles rapid pressure transients and high flow velocity in mountain utility lines.
Industrial Processing & District Heating Integration
Beyond drinking water, Austria's heavy industrial corridors—including paper & pulp processing in Styria, chemical engineering plants in Upper Austria, and biomass district heating systems—require specialized gate valves with chemically inert EPDM elastomeric wedges and corrosion-proof stem materials.
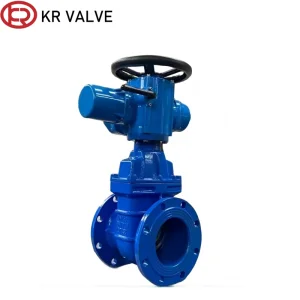
Our factory supplies custom-configured soft seal gate valves equipped with ISO 5211 top flanges for immediate mounting of electric actuators (AUMA, Rotork), enabling seamless automated control in modern Austrian industrial facilities.
- GSK Epoxy Powder Coating: Minimum 250 µm thickness applied electrostatically for non-toxic, anti-corrosive long service life.
- Actuator-Ready Top Flange: Direct mounting according to ISO 5211 for remote SCADA integration.
- Zero-Cavity Bottom Profile: Smooth, un-pocketed channel guarantees smooth sediment passage without wedge obstruction.
Engineering Principles of Our Resilient Seating Technology
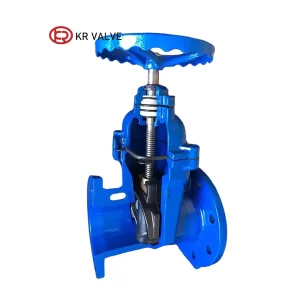
Traditional metal-seated gate valves suffer from debris accumulation in the bottom recess, causing eventual seat erosion and leakage. Our resilient seat gate valve design completely eliminates the bottom seating groove, utilizing advanced rubber vulcanization over a high-tensile ductile iron wedge.
Vulcanized EPDM Wedge
The ductile iron wedge (EN-GJS-500-7) is fully encapsulated with drinking-water grade EPDM elastomer using high-temperature transfer molding. The elastomer formulation is certified under DVGW W270 and UBA guidelines, guaranteeing no microbiological growth or taste alteration in municipal water networks across Austria.
The wedge features internal guide shoes coated with low-friction polyamides, ensuring smooth vertical travel and eliminating coating abrasion during frequent open/close cycles.
Stainless Stem & Stem Nut
The non-rising stem is cold-rolled from high-strength stainless steel (1.4021 / X20Cr13 or 1.4401 / AISI 316 upon request). Cold rolling creates a polished, high-density thread surface that drastically reduces operational torque requirements.
The stem nut is manufactured from dezincification-resistant brass (DZR CW602N) or high-tensile bronze, completely detached from the wedge body to prevent stress concentrations and bending moments on the spindle shaft.
Triple O-Ring Sealing System
Stem sealing is achieved via a primary back-seal ring and multiple independent EPDM O-rings housed in a solid brass sealing gland nut. This maintenance-free design allows shaft seal replacement under full line pressure without shutting down the water main.
A wiper ring located above the primary gland prevents external soil particles, groundwater, and grit from entering the internal stem thread assembly.
Standard Technical Comparison Matrix
Comparing key dimensions, face-to-face standards, and pressure parameters across major valve specifications relevant to Austrian engineers and purchasing managers.
| Specification Parameter | DIN EN 1074 / DIN 3202 F4 | DIN EN 1074 / DIN 3202 F5 | BS 5163 Type A / B | ANSI / AWWA C515 |
|---|---|---|---|---|
| Face-to-Face Standard | EN 558-1 Series 14 (Short) | EN 558-1 Series 15 (Long) | EN 558-1 Series 3 / BS 5163 | ASME B16.10 / AWWA C515 |
| Primary Target Market | Austria, Germany, Central Europe | Austria, Switzerland, Eastern Europe | UK, Commonwealth, Middle East | North America, Global EPC Projects |
| Nominal Diameter (DN) | DN50 – DN600 | DN50 – DN800 | DN50 – DN1200 (2" – 48") | DN50 – DN600 (2" – 24") |
| Pressure Rating | PN10 / PN16 / PN25 | PN10 / PN16 / PN25 | PN10 / PN16 / PN25 | Class 150 / 250 PSI / 300 PSI |
| Flange Drilling | EN 1092-2 PN10/16/25 | EN 1092-2 PN10/16/25 | BS EN 1092-2 Table E/D/PN16 | ASME B16.1 / B16.42 Class 125/150 |
| Body & Bonnet Casting | Ductile Iron EN-GJS-400-15 | Ductile Iron EN-GJS-500-7 | Ductile Iron EN-GJS-400-15 | Ductile Iron ASTM A536 65-45-12 |
| Internal & External Coating | GSK Epoxy Powder (≥250 µm) | GSK Epoxy Powder (≥250 µm) | Fusion Bonded Epoxy (FBE) | AWWA C550 Compliant FBE |
| Underground Burial Compatibility | Fully Compatible | Fully Compatible | Fully Compatible | Fully Compatible |
Macro-Industry Solutions for Austrian Infrastructure Projects
Tailored engineering packages designed to resolve complex flow control challenges across Austria’s topography, municipal utilities, and industrial sectors.
Deep Underground Burial & Extension Spindles
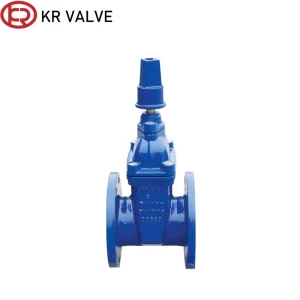
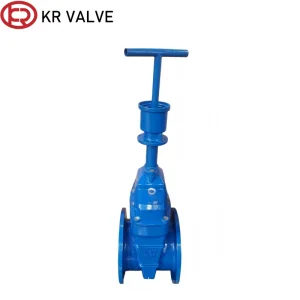
In Austrian municipal water supply networks, gate valves are frequently installed deep underground below the frost line (up to 1.8 to 2.5 meters depth). We manufacture complete underground kits including rigid or telescopic extension spindles, street covers (ÖNORM compliant surface boxes), and T-key operating keys.
Our stem protection tubes feature moisture-proof PE casing seals that prevent subsoil water ingress into the valve stem cap assembly, ensuring light operation even after decades of burial.
Request Underground Extension CatalogKey Customization Options Available
- Handwheel, Cap, or Actuator Drive: Handwheel in ductile iron/steel, square cap for T-key operation, or ISO 5211 gear/electric motor flange.
- Bypass Valve Integration: DN350 and larger gate valves can be fitted with integrated side bypass valves to equalize differential pressure prior to opening.
- Position Indicator & Limit Switches: Mechanical or inductive position sensors for automated feedback to central control rooms.
- High-Pressure PN25 Castings: Heavy-wall GGG50 body castings reinforced for mountainous high-head pipeline applications.
Technology Roadmap & Next-Generation Valve Innovations
Aligned with the European Union’s Green Deal and digital infrastructure goals, our R&D engineering team is advancing smart flow control technologies tailored for Austria and the broader EU market.
IoT Smart Stem Caps (2025–2027)
Integrating wireless multi-sensor stem caps that measure internal line pressure, fluid temperature, rotational count, and real-time open/close percentage without external cabling. Battery-powered modules transmit data via NB-IoT directly to municipal utility SCADA dashboards.
Lead-Free Eco-Brass Components
Transitioning all stem nuts and internal brass components to 100% lead-free alloy compositions (CuZn21Si3P / CW724R), anticipating stricter EU Drinking Water Directive chemical limits and ensuring zero heavy metal leaching in drinking water systems.
Low-Carbon Manufacturing & Recycling
Utilizing electric arc furnace (EAF) melted ductile iron scrap material with 100% green energy sourcing. Eco-friendly powder coatings free of VOCs and heavy metals ensure complete environmental compliance under EU REACH regulations.
Technical & Procurement FAQ for Austrian Buyers
Direct answers to technical questions commonly submitted by consulting engineers, utility procurement managers, and industrial valve distributors across Austria.
What is the structural difference between DIN F4 and DIN F5 resilient seat gate valves?
The fundamental difference lies in their face-to-face overall length as defined by EN 558-1 standard. DIN F4 corresponds to Series 14 (short pattern), offering a compact footprint ideal for retrofitting existing plant rooms or compact manholes. DIN F5 corresponds to Series 15 (long pattern), providing a wider body footprint that offers enhanced flow stabilization and extra body mass, frequently preferred for high-pressure municipal mains across Austria and Germany.
How do your valves comply with ÖVGW and European drinking water regulations?
Our resilient seat gate valves are constructed strictly according to EN 1074-1 and EN 1074-2 standards. All internal elastomeric components utilize high-purity EPDM rubber that holds DVGW W270 and UBA elastomer approval certification. The electrostatic epoxy coating is applied at a minimum thickness of 250 µm under strict GSK rules, ensuring zero organic leaching and zero bacterial growth in drinking water pipelines.
Can resilient seat gate valves withstand alpine freeze-thaw cycles in Austria?
Yes. The valve bodies are cast from high-grade Ductile Iron EN-GJS-400-15 / EN-GJS-500-7, which offers superior impact resistance and tensile yield strength compared to standard gray cast iron. When installed with our underground extension spindles and proper gravel backfill below frost lines, the resilient wedge absorbs ambient ground thermal stresses without binding or cracking.
What factory quality testing is performed prior to dispatching orders to Austria?
Every single valve undergoes 100% hydrostatic factory testing in compliance with EN 12266-1. Shell testing is conducted at 1.5 times nominal pressure (e.g., 24 bar for PN16), and seat leakage testing is executed at 1.1 times nominal pressure (17.6 bar for PN16) under Rate A zero-leakage standards. Low-pressure seat air testing (0.5 bar) is also performed to verify low-pressure elastomeric seal integrity.
Do you support OEM branding and customized flange drilling for European EPC buyers?
Yes. We offer complete OEM services for distributors, valve stockists, and EPC contractors. Custom options include private-label nameplate riveting, specific RAL paint color coding (e.g., RAL 5005 for water, RAL 7011 for industrial wastewater), custom stem extension lengths, and flange drillings to EN 1092-2 PN10, PN16, PN25, or ANSI Class 150.
What is the typical production lead time and freight logistics setup for Austria?
Standard DIN F4/F5 catalogue items (DN50 to DN300) are maintained in stock for rapid dispatch. Custom engineered orders or large project lots generally require 25 to 35 days production lead time. Shipments are packed in export-grade seaworthy wooden cases with moisture barrier wrapping and delivered via direct maritime container freight to European ports (Rotterdam, Koper, Hamburg) followed by direct overland truck transport into Austria.
Explore Our Full Gate Valve & Flow Control Range
Extensive lineup of rising stem, non-rising stem, underground, electric actuated, ball check, and PTFE lined industrial valves available for direct factory shipment to Austria.